

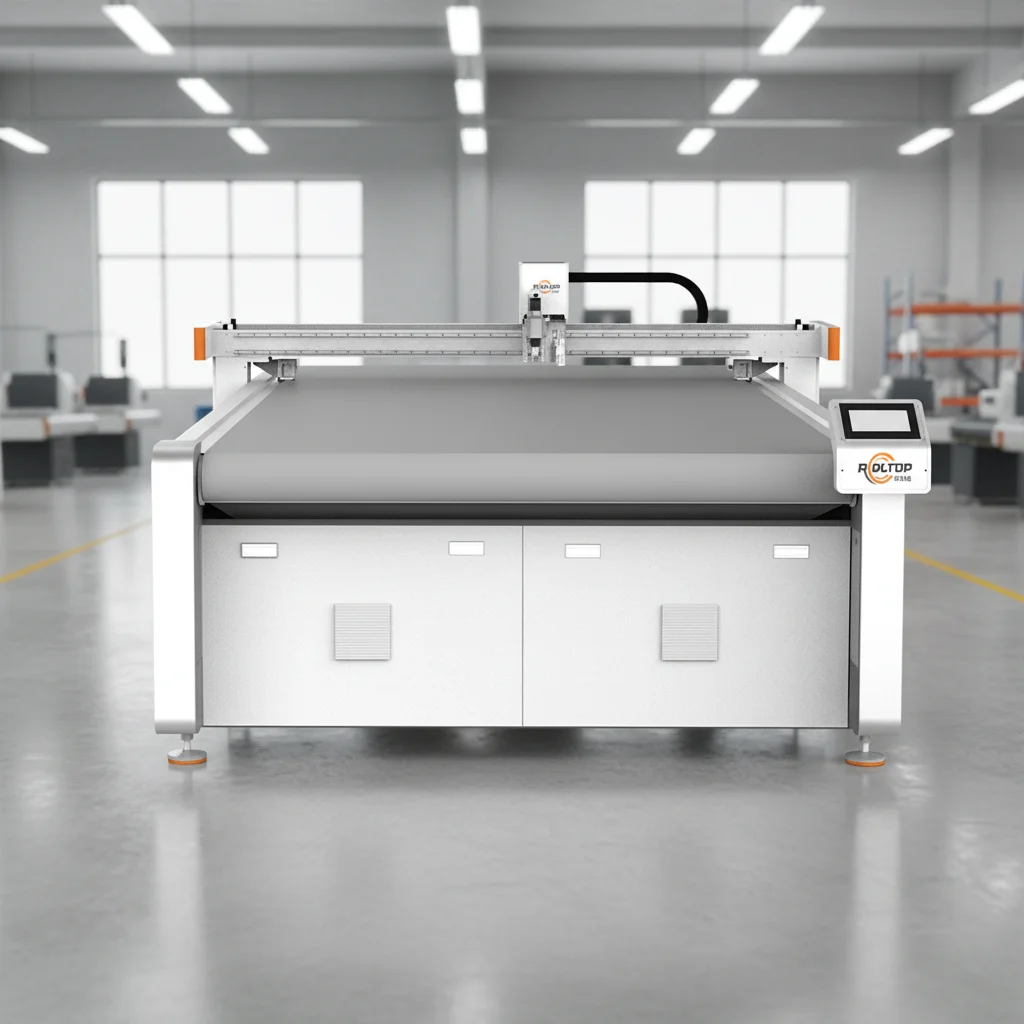
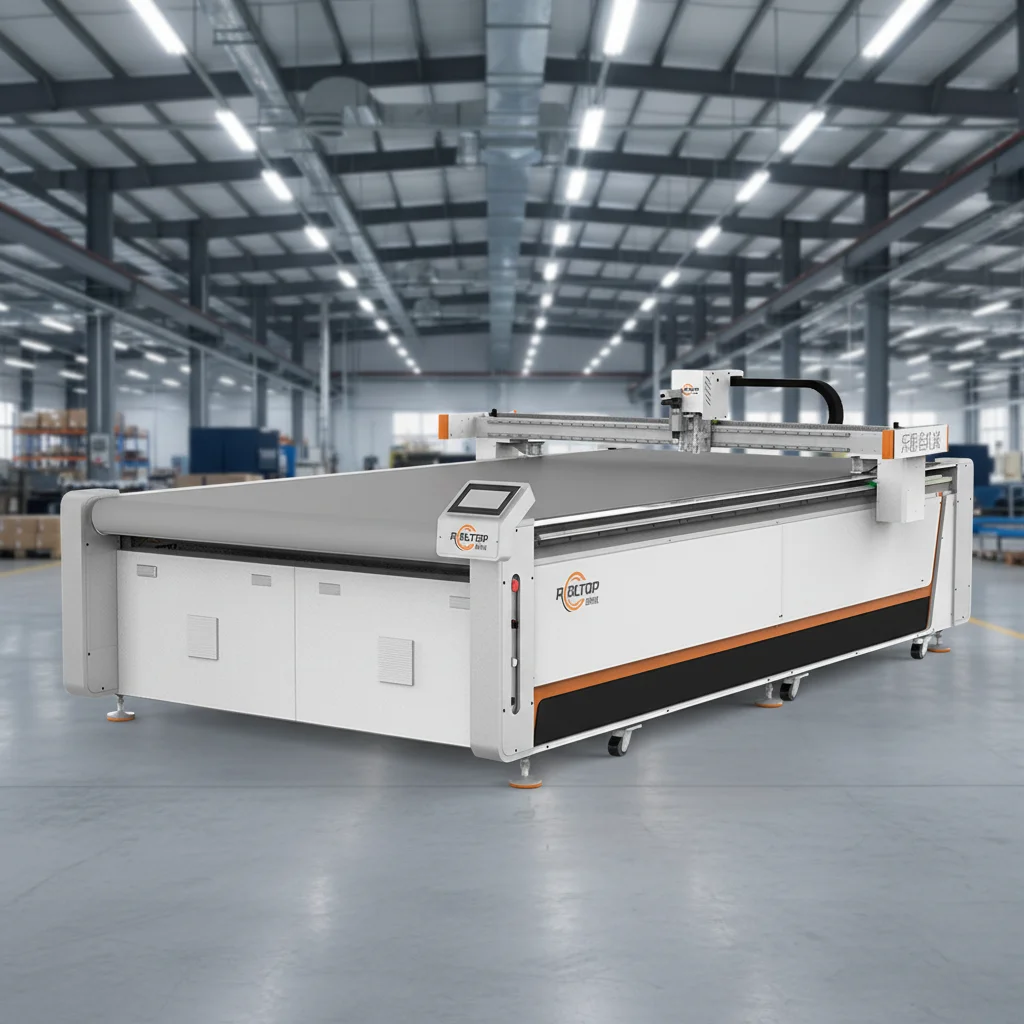
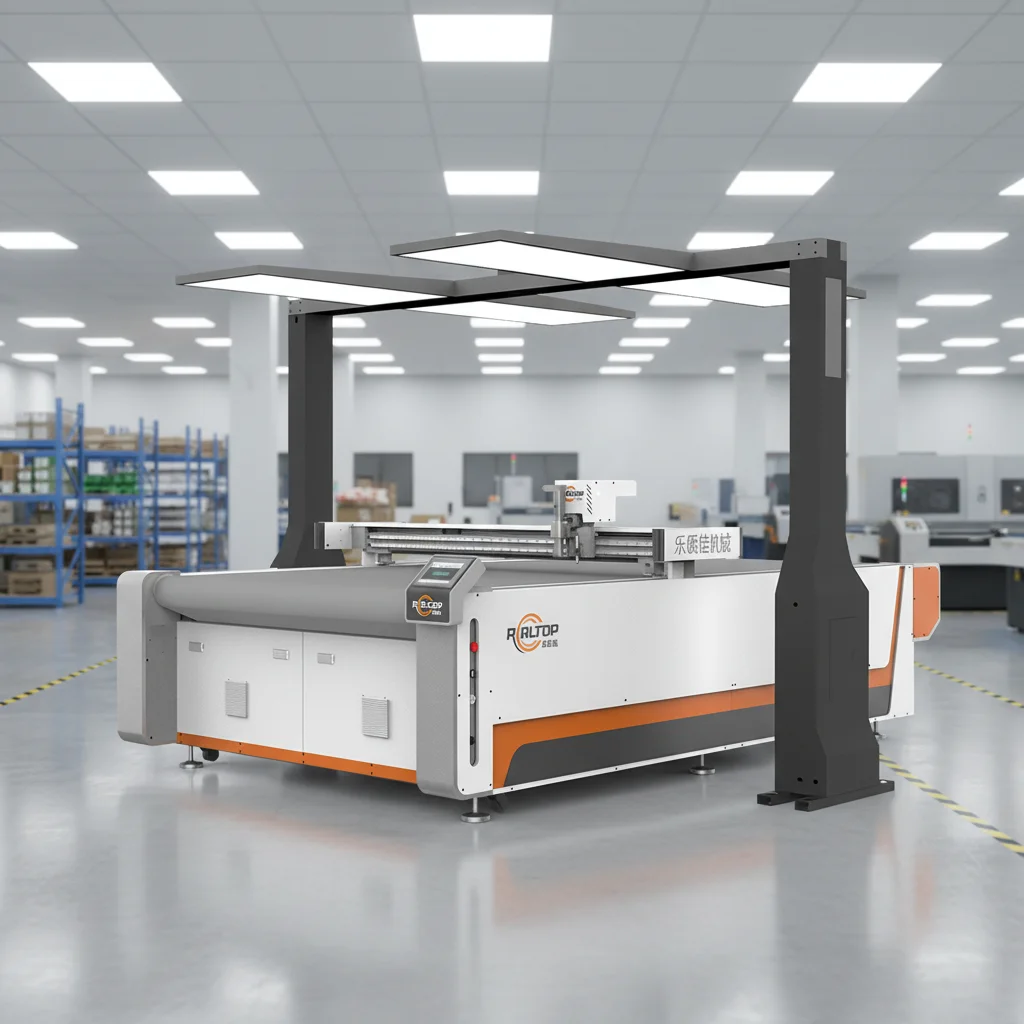
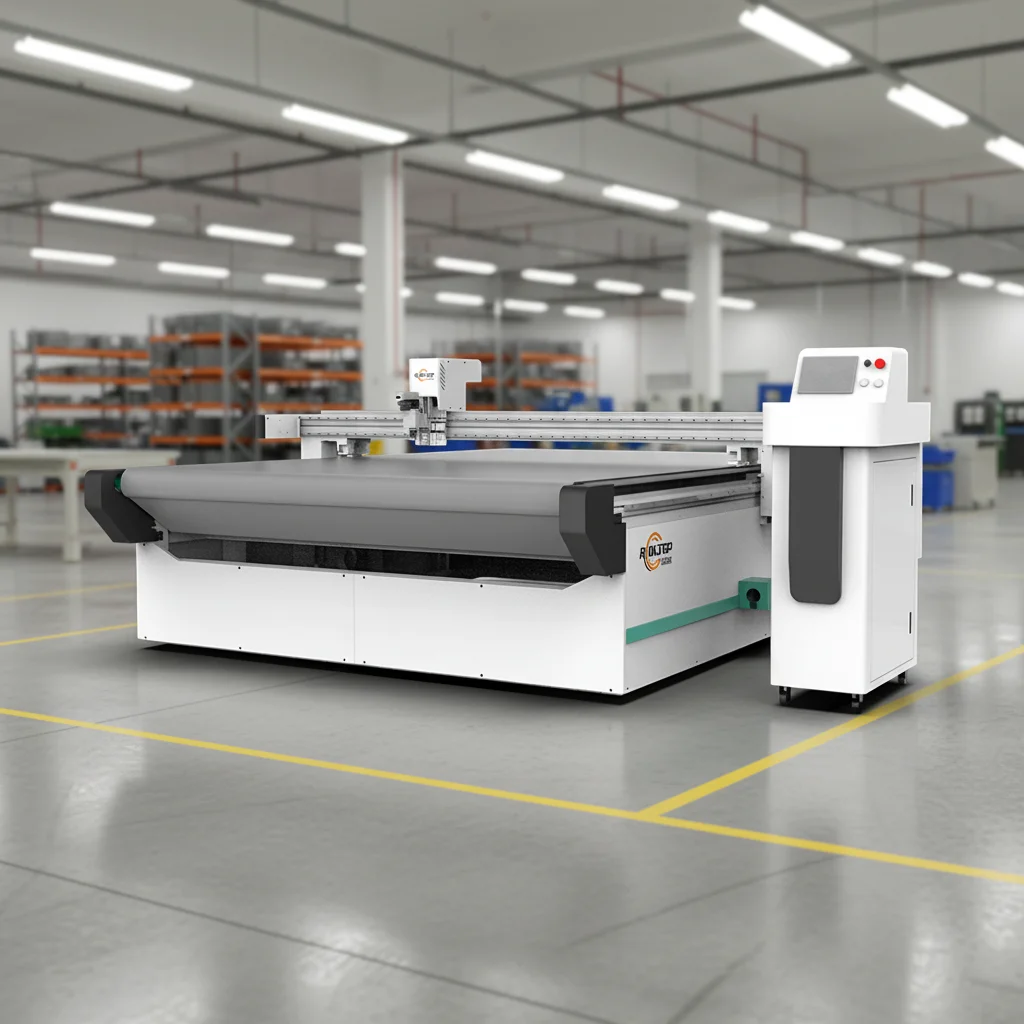
Fabric Multi-Layer Vibrating Knife Cutter – Specifications
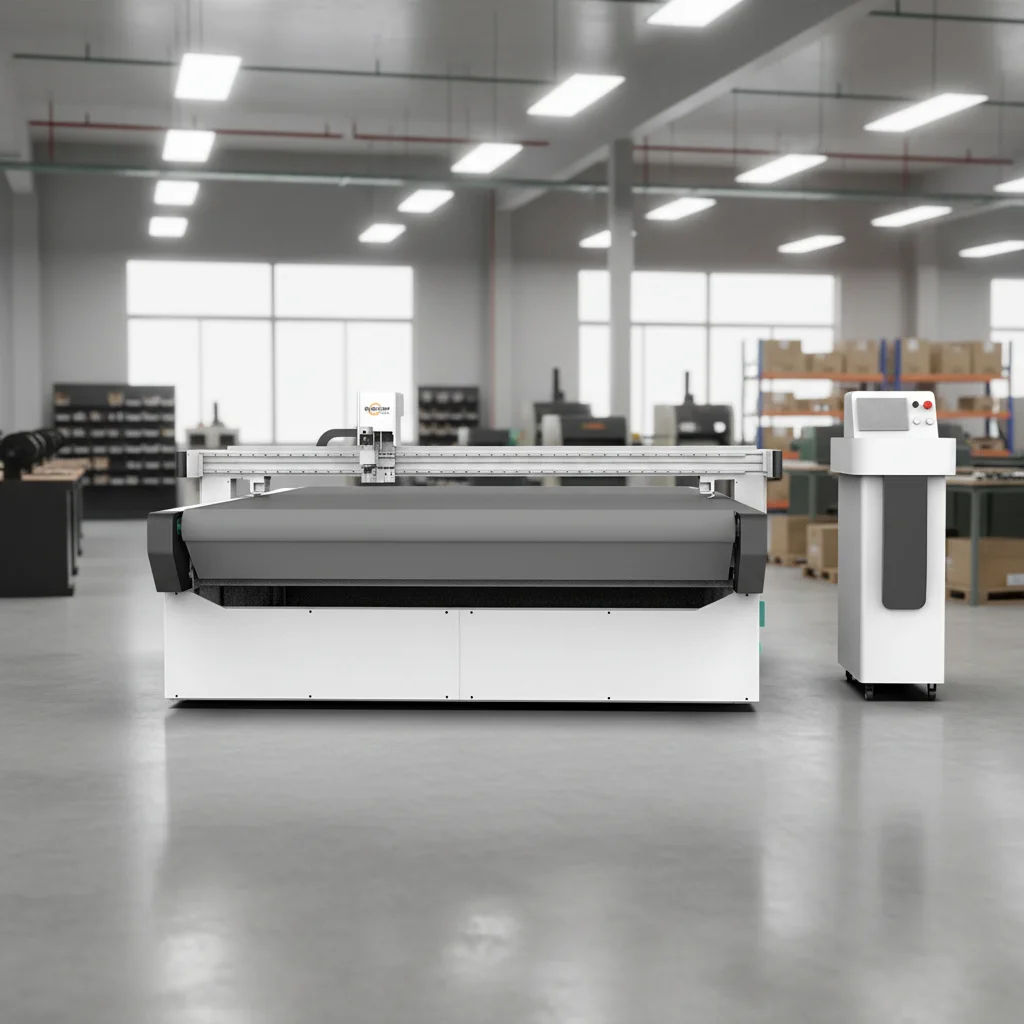
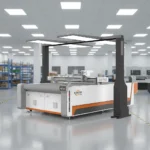
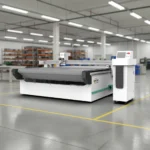
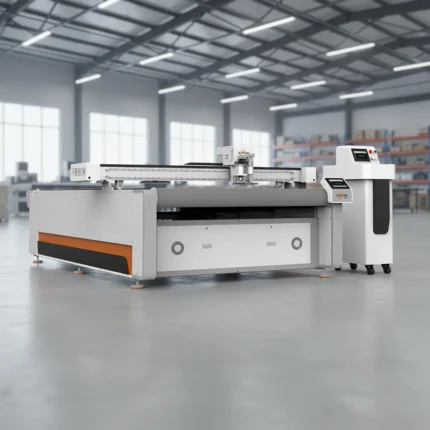
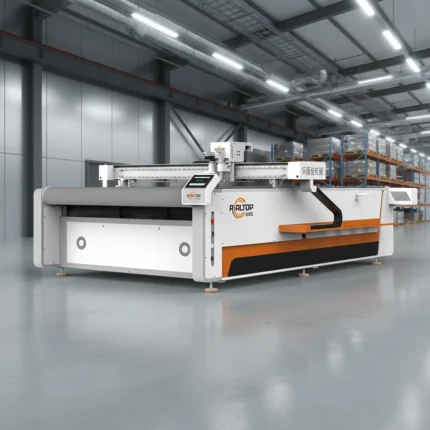
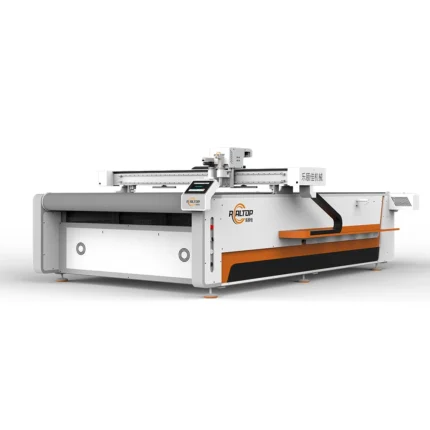
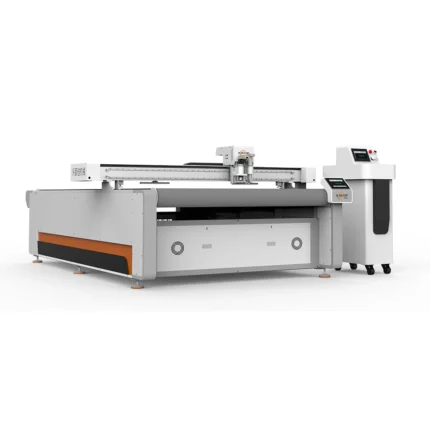
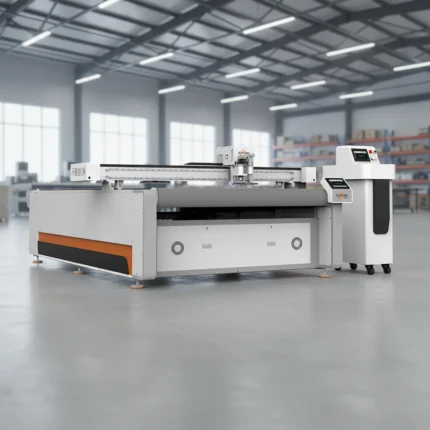
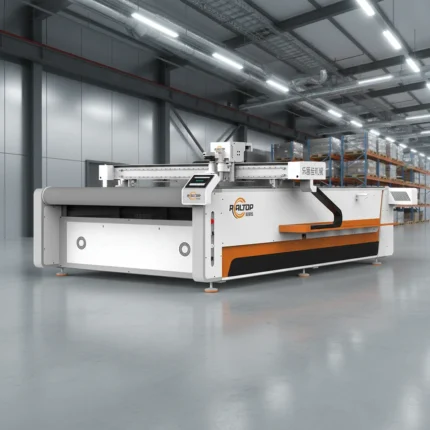
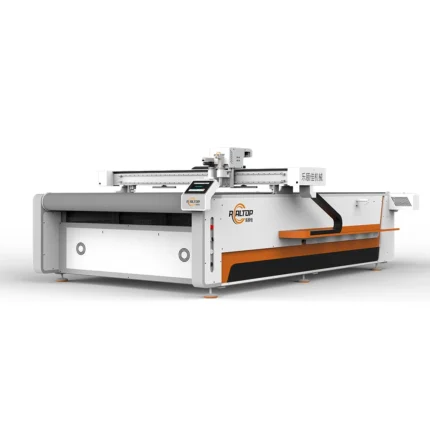
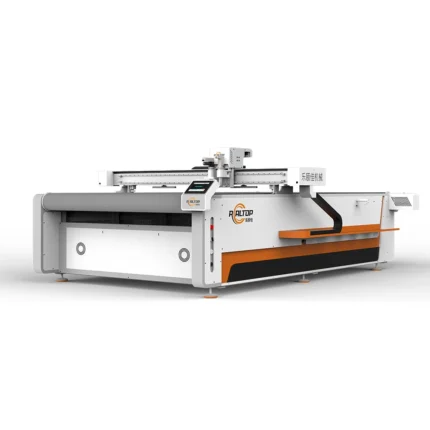
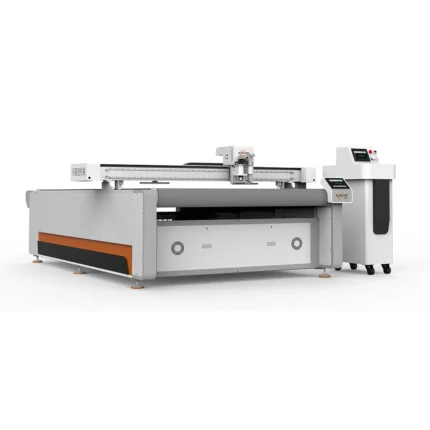
1625 CNC Oscillating Knife Cutting Machine, 1600×2500mm working area, ≤30mm cutting thickness — configured for fabric and composite cold cutting where CO2 laser leaves scorched edges or toxic fumes.
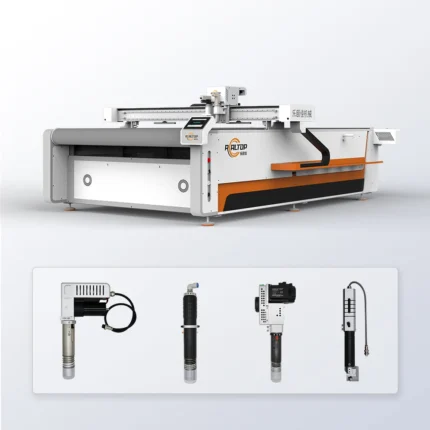
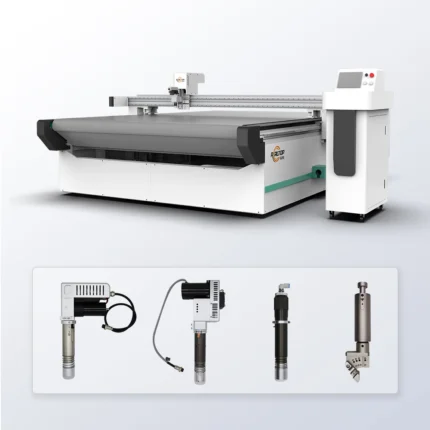
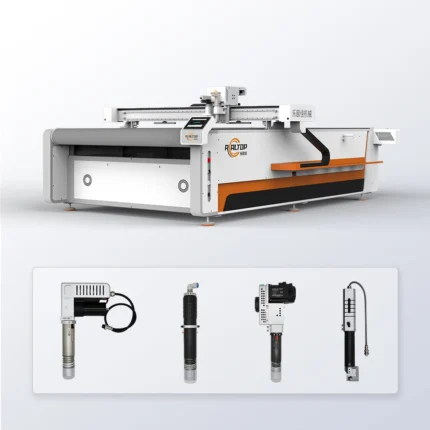
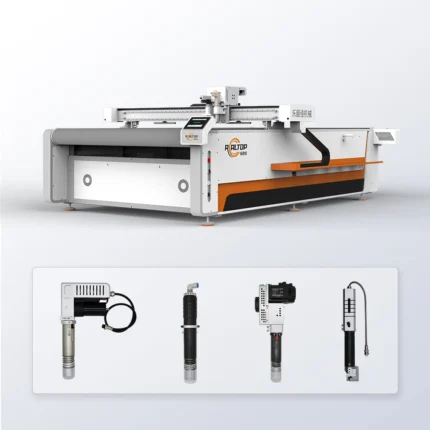
- Interchangeable tool heads (oscillating knife, driven rotary, pneumatic knife) matched to material type
- Aluminum bellows vacuum table with 9kW pump ensures stable multi-layer hold-down
- ±0.1mm cutting accuracy across flexible substrates
- File format compatibility: PLT, DXF, AI, PDF
Sample cutting on your own material validates edge quality before commitment, with voltage and control language confirmed to your market.
Cold-Cutting Precision — Tool head and table configuration specified per material and production volume to eliminate thermal damage on synthetics and multi-layer textiles.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | 1625 |
| Product Type | CNC Oscillating Knife Cutting Machine |
| Working Area | 1600×2500 mm |
| Tool Head Options | Oscillating knife, Driven rotary knife, Creasing wheel, Kiss cutting tool, Pneumatic knife, Milling tool, V groove knife |
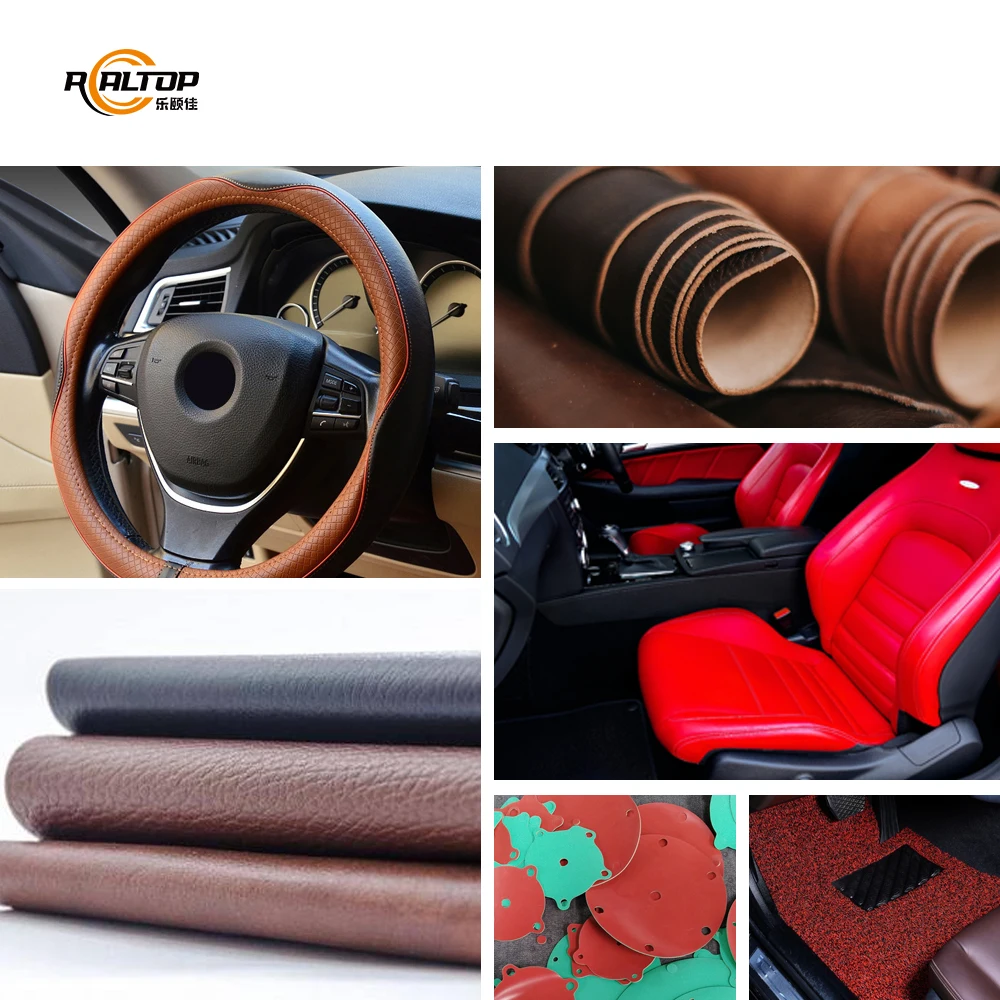
| Applicable Materials | Fabric, Cardboard, Carton, Mats, PVC, EVA, Leather, Acrylic, Foam, PTFE, Rubber |
| Cutting Speed | 0–2000 mm/s (basis not stated in source — confirm material / thickness / layer count) |
| Cutting Thickness | ≤ 30 mm (basis not stated in source — confirm material type and layer configuration) |
| Cutting Accuracy | ±0.1 mm |
| Vacuum Pump | 9 kW |
| Vacuum Table | Aluminum bellows vacuum table |
| Control System | PLC control panel with optional display languages |
| Language Options | English, Russian, Italian, Chinese; special languages customizable |
| Servo Drive Options | Panasonic, Delta, Dorna (source value — verify against manufacturer catalog) |
| File Formats Supported | PLT, DXF, AI, PDF |
| Voltage Options | 110V, 220V, 380V (frequency not specified in source) |
| Safety Device | Infrared sensor device and emergency stop device |
| Machine Size | 3300×2100×1350 mm |
| Certification | CE (specific standard number not stated in source) |
Application Suitability
| Application | Material or Output |
|---|---|
| Apparel manufacturing | Suits, knitwear, lace, complex patterned fabrics with pattern-matching layouts |
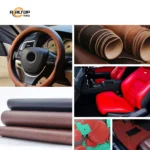
| Automotive interiors | Seat fabrics, carpets, PVC mats with burr-free edge requirements |
| Home textiles | Multi-layer sofa fabrics, curtains, rugs with vacuum hold-down |
| Composite material processing | Carbon fiber prepreg, aramid, specialty flexible materials without delamination or thermal deformation |
Why Edge Sealing Is Not Always the Right Answer for Synthetics
A cold knife process produces zero thermal distortion on foam, elastane blends, or technical textiles where a CO2 beam would melt, yellow, or fuse the fibers.
When a laser cuts multi-layer spandex or foam, the heat seals the edge — but also shrinks the surrounding fabric, warps the cut path, and releases fumes that require extraction infrastructure. I once spent three days on the shop floor re-dialing power, speed, and assist gas for an elastane blend because the cotton test samples looked perfect while the actual production rolls curled and scorched. A CNC oscillating knife cutting machine laser process alternative removes the thermal variable entirely, cutting through flexible composites and stretch textiles without melting or discoloration. This matters most when the edge must remain open for subsequent sewing, bonding, or coating steps [NEED_CITE: cold cutting versus thermal cutting for elastomeric textiles].
Thermal Damage Versus Mechanical Separation
CO2 lasers excel on materials that benefit from a sealed edge, such as acrylic or polyester fleece, where the beam cauterizes the fibers and prevents fraying. On polyurethane foam, elastane-blended knits, or prepreg composites, that same heat creates a hardened bead along the cut line, delamination between layers, or discoloration on light-colored technical fabrics. A CNC oscillating knife cutting machine laser process alternative achieves mechanical separation — the blade physically shears through the material, leaving the fiber structure unaltered on both sides of the kerf.
Multi-Layer Stacking Without Thermal Accumulation
Cutting a single ply of fabric with a laser is straightforward. Stacking ten or twenty plies and cutting through the full stack introduces compounding thermal effects: the beam dwells longer on inner layers, edges fuse together, and the bottom ply may scorch before the top ply is fully severed. The 1625 knife cutter, paired with a 9 kW vacuum pump and aluminum bellows vacuum table, holds multi-layer lays flat and stable while the oscillating knife traverses the full 30 mm depth in a single pass [NEED_CITE: multi-layer textile cutting practices in automotive upholstery production].
Tool Head Selection by Material Response
Each tool head option addresses a distinct material behavior. The oscillating knife handles dense woven fabrics and foam with a high-frequency vertical stroke that prevents drag and fraying. The driven rotary knife suits continuous long cuts on vinyl and PVC where a clean, unbroken edge is required. The kiss cutting tool scores adhesive-backed films without penetrating the release liner. The creasing wheel scores cardboard and carton for folding. Choosing the correct head prevents ragged edges, crushed foam cores, and delaminated composite plies — issues that cannot be corrected downstream.
How Vacuum Zoning and Accuracy Tolerances Affect the Cut
The aluminum bellows vacuum table paired with a 9 kW pump generates sufficient hold-down force to keep flexible materials from lifting during high-speed traverse, which is especially critical for small pattern pieces that tend to drift when the tool head changes direction. The ±0.1 mm cutting accuracy means nested parts — such as automotive seat panels or garment pieces cut from the same lay — maintain dimensional consistency across the full 1600×2500 mm working area. For production environments running hundreds of plies per shift, this repeatability prevents cumulative tolerance drift that would otherwise surface as misaligned seams or ill-fitting assembled components.
File format compatibility with PLT, DXF, AI, and PDF eliminates the intermediate conversion step that often introduces geometry errors in nesting workflows. The PLC control panel, configurable with English, Russian, Italian, or Chinese display language, reduces operator error when the production floor staff are not native English speakers [NEED_CITE: operator language configuration in exported CNC equipment].
The Cost of Misconfigured Tooling and Unverified Voltage
Selecting a tool head based on catalog description rather than actual material samples is one of the most common procurement errors in cold cutting. An oscillating knife set at the wrong stroke frequency for a specific foam density will crush the core instead of shearing it, producing a visibly deformed edge that fails quality inspection. Similarly, ordering a machine at 380V for a facility wired for 220V single-phase — or failing to confirm the local frequency standard — means the servo drives and vacuum pump will either trip protection circuits immediately or operate at degraded torque, which shows up as inconsistent cutting depth and positioning drift after several hours of production [NEED_CITE: voltage and frequency standards by export market].
Why This Sourcing Approach Reduces Field Failures
In-house design and production covering both knife and laser technologies means the cutting method is matched to the material rather than forced through one process. Every tool head and table configuration is specified per the buyer’s material type and daily production volume, not offered as a default package. Sample cutting on the buyer’s own material is completed before commitment, so edge quality is validated against a physical benchmark rather than a brochure claim. Voltage, plug type, control language, and software file format are confirmed in writing before production begins, preventing shipment of equipment that cannot power on or import existing nesting files.
Documentation & Verification
- Machine specification sheet listing confirmed tool head and table configuration for your material
- Electrical schematic with voltage and frequency matched to your facility before build
- Sample cutting report on your actual fabric or composite material before order confirmation
- Software licence and file format compatibility note for your existing PLT or DXF nesting workflow
- Factory test record demonstrating cutting accuracy and vacuum hold-down under load
- Packing photographs documenting machine condition at the point of dispatch
Installation, Commissioning & Support
- Machine footprint of 3300×2100 mm requires a level concrete floor with clearance for material loading on both long sides
- 9 kW vacuum pump and servo drives require a dedicated circuit matching the confirmed 110V, 220V, or 380V supply
- Machine ships as a single assembled unit; rigging and positioning must accommodate the full machine size
- First-run commissioning includes tool head stroke calibration and vacuum zone balancing for your specific material
- Operator training covers PLC panel navigation in the confirmed display language and tool head changeover procedure
- Spare parts list identifies consumable blades, knife holders, and vacuum table seals by part number
Preparing Your Inquiry for an Accurate Quotation
To receive a configuration and quotation that matches your production environment, provide the material type, thickness, maximum sheet or roll width, and the number of plies or layers you intend to cut per pass. Specify the local voltage and frequency standard, the required control panel language, and the nesting software or file format currently in use. If edge quality on a specific substrate is critical — for example, burr-free cuts on automotive PVC mats or fray-free edges on aramid composites — request sample cutting on your own material before confirming the order.
Frequently Asked Questions
Q: When should I choose cold knife cutting over a CO2 laser for fabric?
A: Cold knife cutting is the correct choice when the material is heat-sensitive — such as elastane blends, polyurethane foam, or prepreg composites — where a laser beam would melt fibers, discolor edges, or cause delamination. It is also preferred when the cut edge must remain open for sewing or bonding. A CO2 laser is better suited to materials that benefit from a sealed, cauterized edge.
Q: What material and thickness does the 30 mm cutting depth apply to?
A: The maximum cutting thickness of 30 mm depends on the material density, layer count, and tool head selected. Soft, low-density foams can be cut at full depth with an oscillating knife, while dense woven fabrics or composites may require reduced layer counts. Sample cutting on your specific material is the only reliable way to confirm achievable depth and edge quality.
Q: Will the machine accept my existing nesting files?
A: The control system supports PLT, DXF, AI, and PDF file imports. Before the order is confirmed, a software licence and file format compatibility note is issued to verify that your existing nesting workflow imports correctly without geometry conversion errors or missing layers.
Q: Can the voltage and control language be matched to my local standard?
A: Voltage options include 110V, 220V, and 380V, with frequency confirmed during the ordering process. The PLC control panel display language is configurable to English, Russian, Italian, or Chinese, and special languages can be customized. All electrical specifications are confirmed in writing before production begins.
Q: How do I verify edge quality before committing to a purchase?
A: A sample cutting report is produced on your own material — the exact fabric, foam, or composite you will run in production — documenting the tool head used, cutting parameters, and resulting edge condition. This physical benchmark is compared against your quality standard before the machine order is finalized.


Related products
2026 Máquina de corte de tela CNC automática Plotter de tela y cuero de alta precisión
Product Introduction
2026 Auto CNC Cloth Cutting Machine, a high-precision fabric & leather plotter designed for efficient cutting. Ideal for textile and leather industries with advanced CNC technology.
Key Specifications
| Model | Auto CNC Cloth Cutting Machine 2026 |
| Application | Fabric & Leather |
| Precision | High-Precision Cutting |
| Type | CNC Plotter |
Máquina de corte automático de tela 1200mm Delta Servo 2026
Product Parameters
| Cutting Width | 1200mm |
| Servo System | Delta Servo |
| Model Year | 2026 |
Introduction
High-performance Automatic Fabric Cutting Machine with 1200mm cutting width, equipped with Delta Servo for precision. Ideal for efficient fabric processing in textile industry, ensuring accurate and fast cutting operations.
Sistema de Cuchilla Vibratoria CNC 2026 para Prepreg No Tejido de Poliéster y Nailon
Product Introduction
CNC Vibration Knife System 2026 is ideal for cutting polyester, nylon, non-woven fabrics, and prepreg materials with precision and efficiency, suitable for industrial manufacturing needs.Product Parameters
| Model | 2026 |
| CNC Vibration Knife | |
| Materials | Polyester, Nylon, Non-Woven, Prepreg |
Máquina de Corte de Tela CNC Realtop 2026 Certificada CE
Product Introduction
Realtop CNC Fabric Cutting Machine 2026, CE Certified, ideal for precision fabric cutting with advanced CNC technology. Engineered for efficiency and reliability in textile manufacturing processes.Key Specifications
| Model | Realtop CNC Fabric Cutting Machine 2026 |
| Certification | CE Certified |
商品评价
There are no reviews yet.