


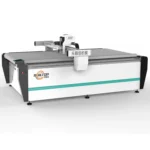
Apparel Machinery Auto Fabric Cutter for Multi-Layer – Full Range
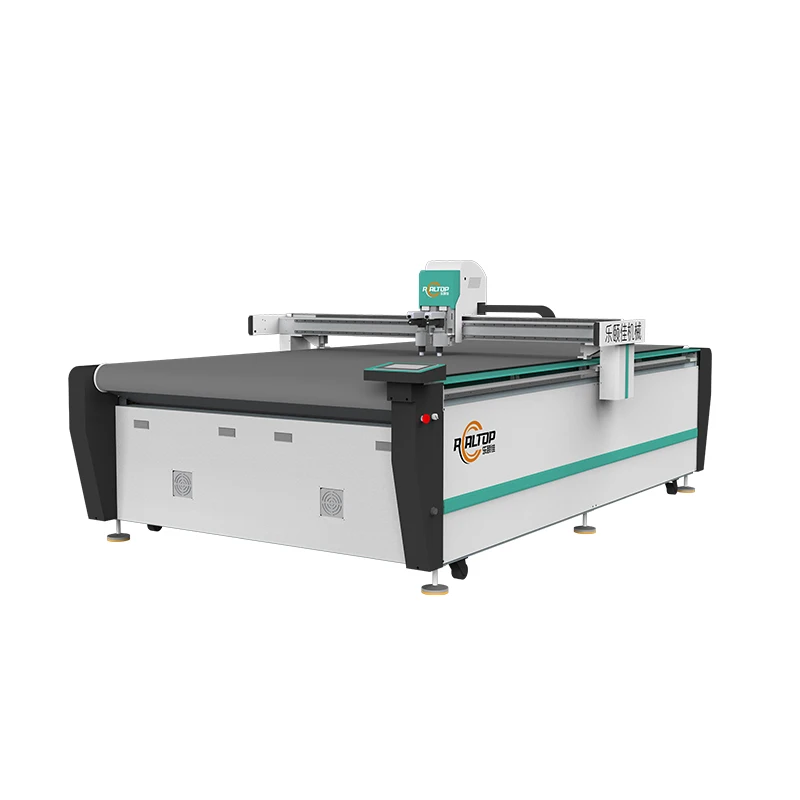
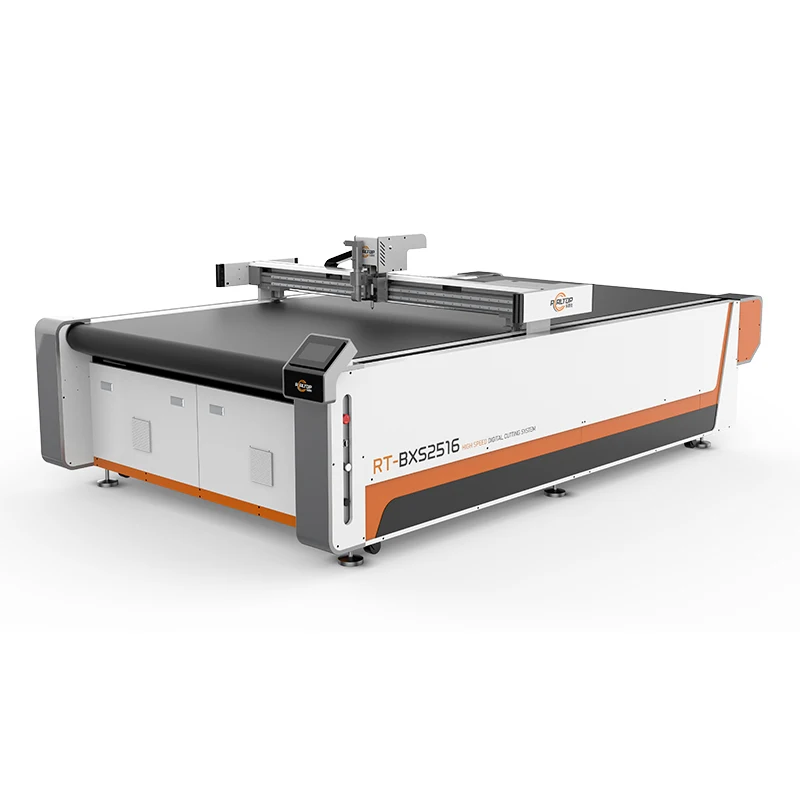
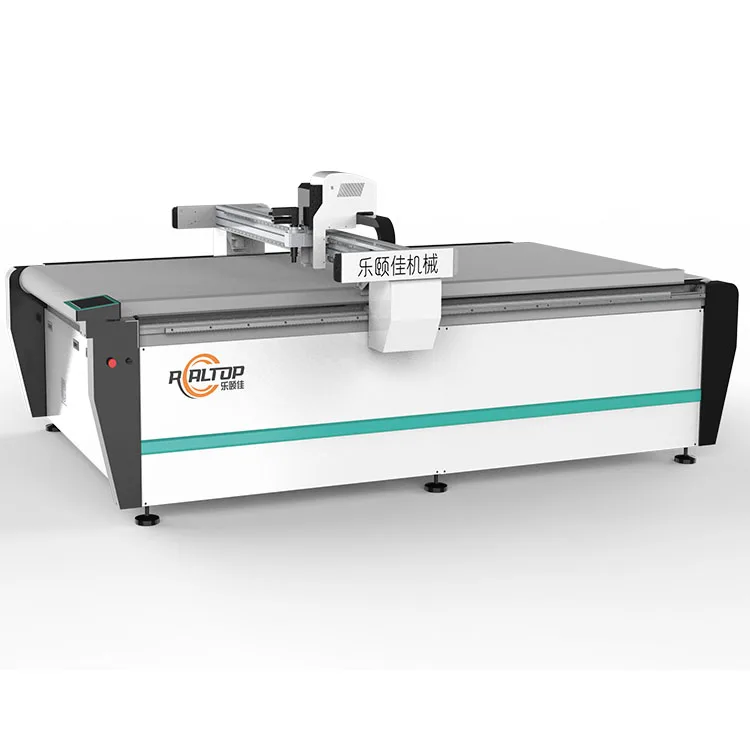
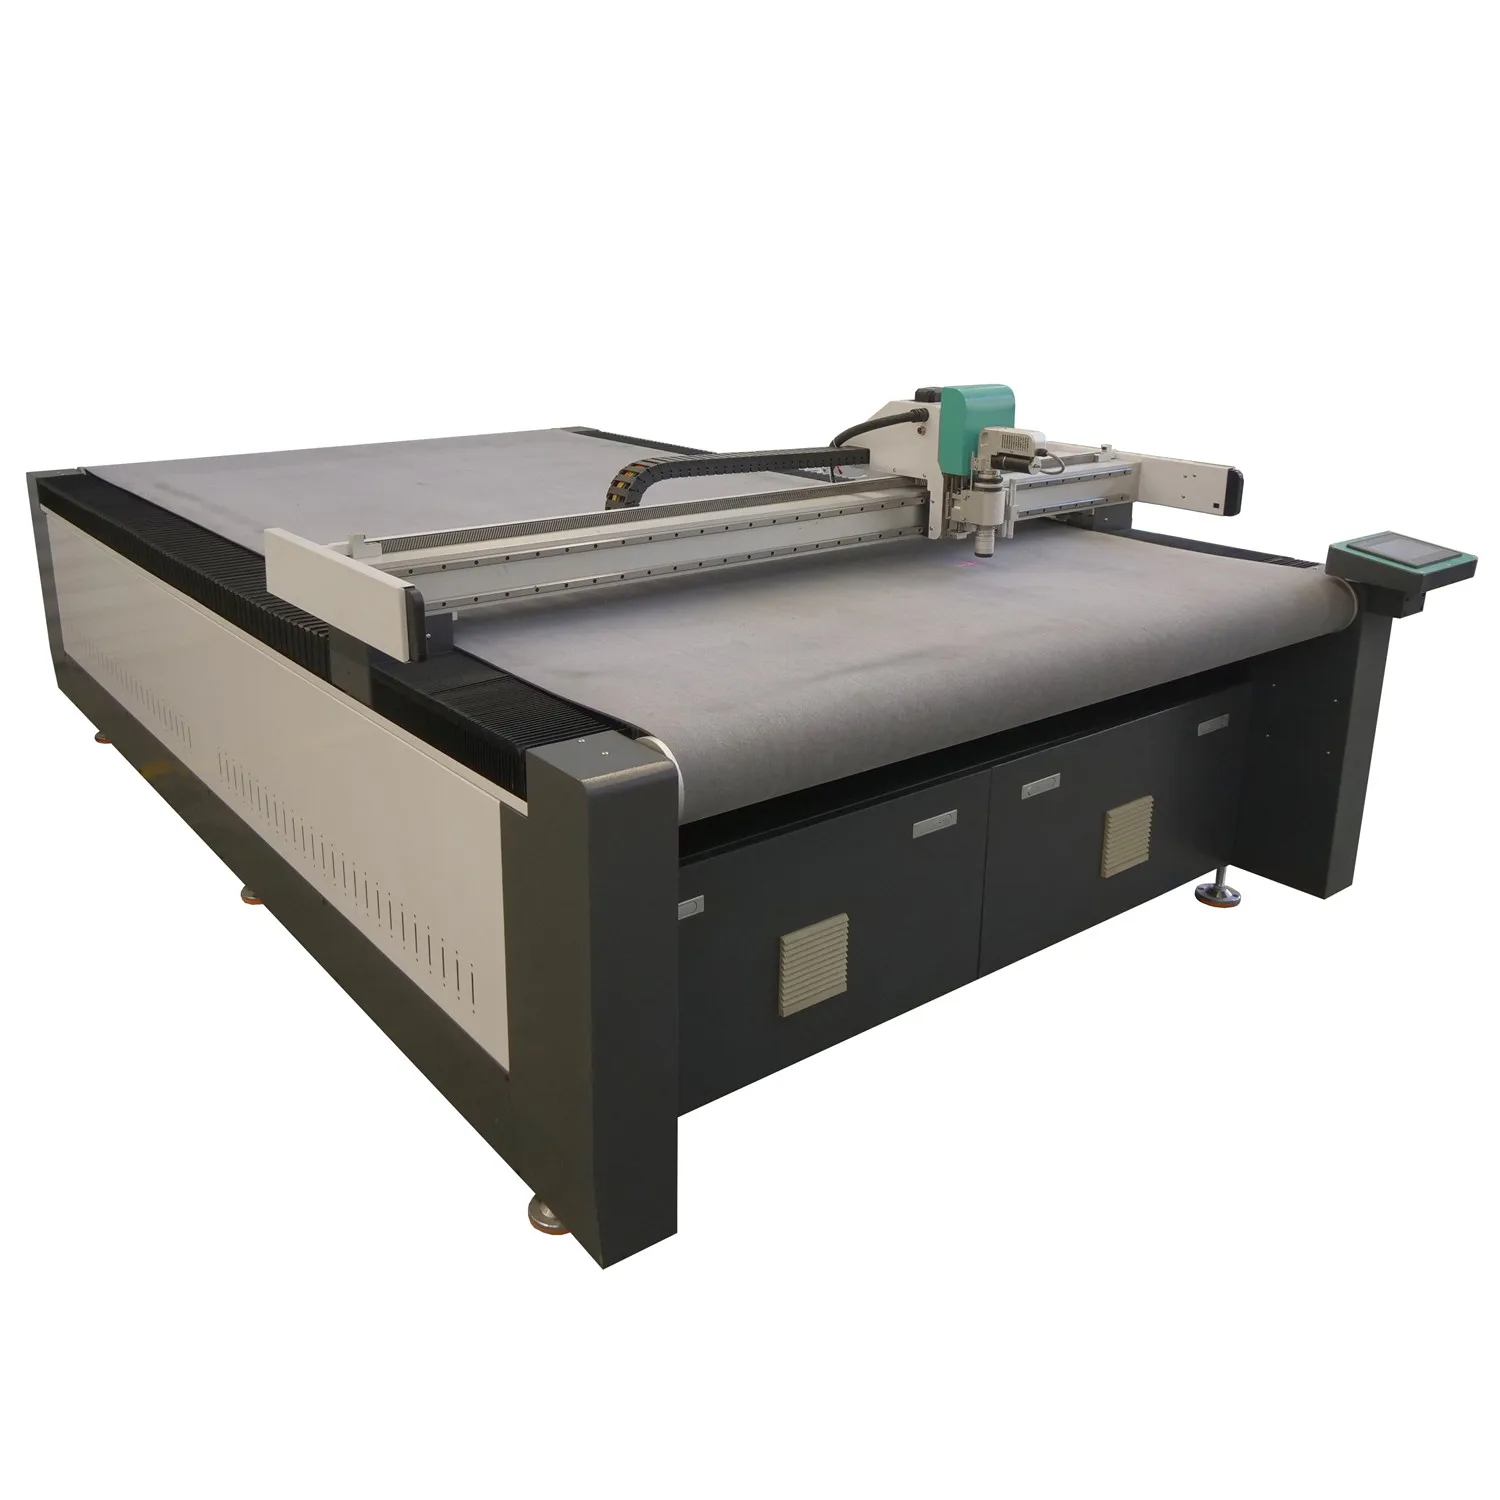
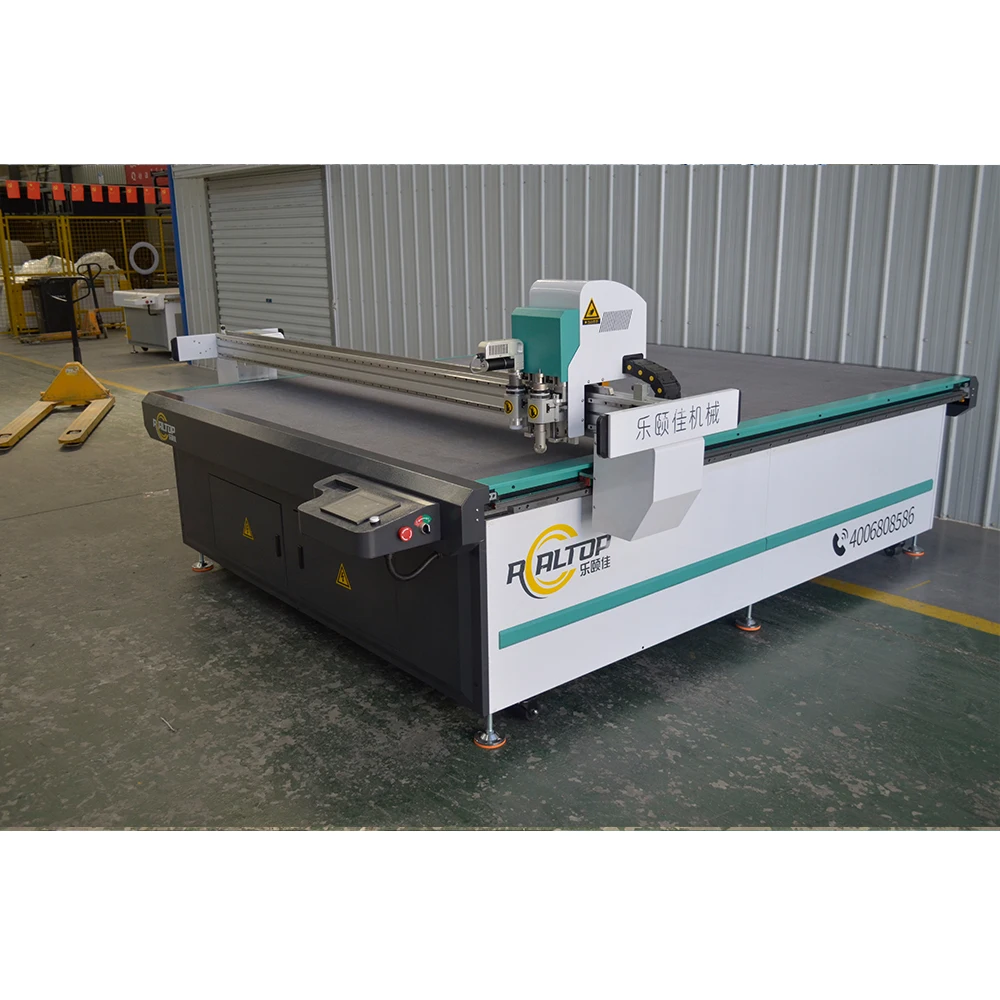
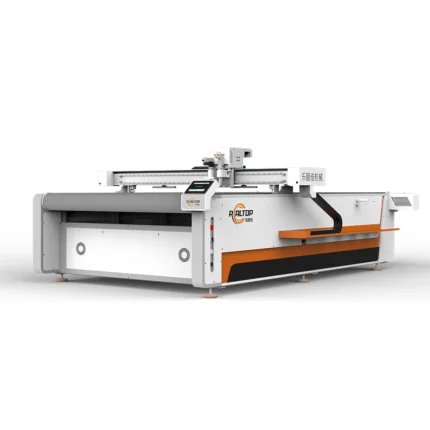
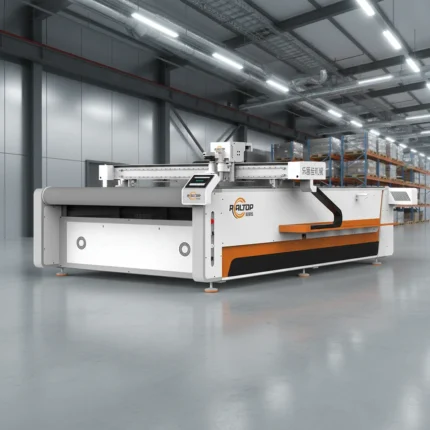
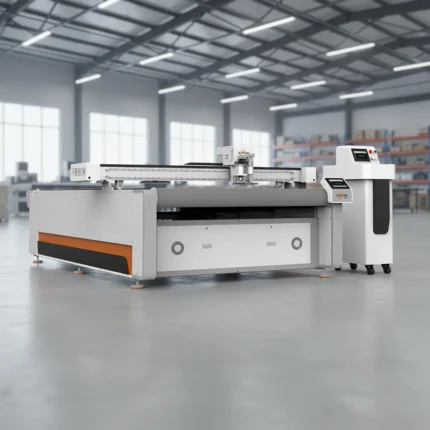
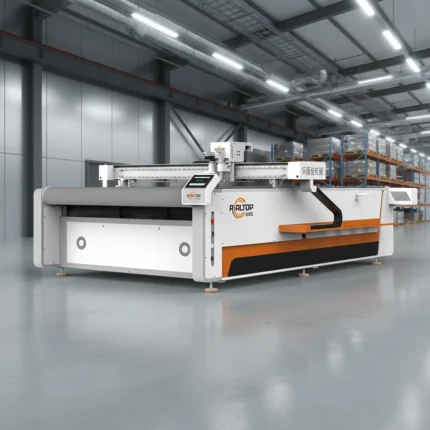
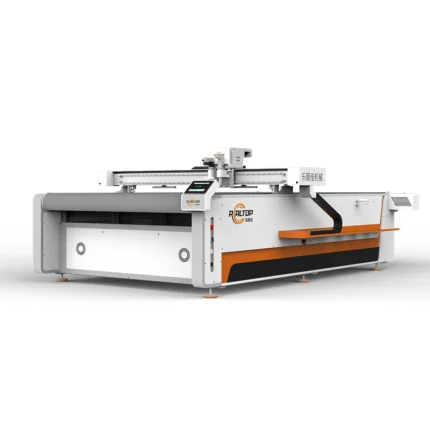
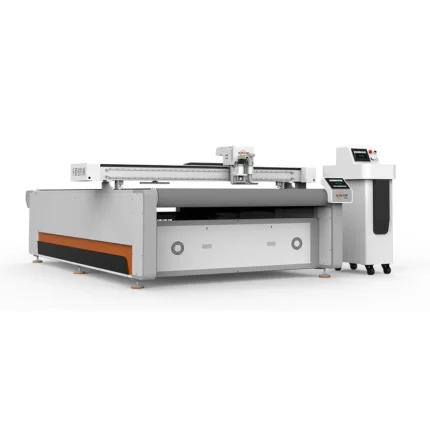
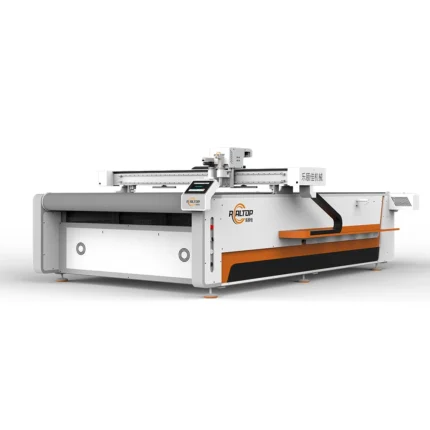
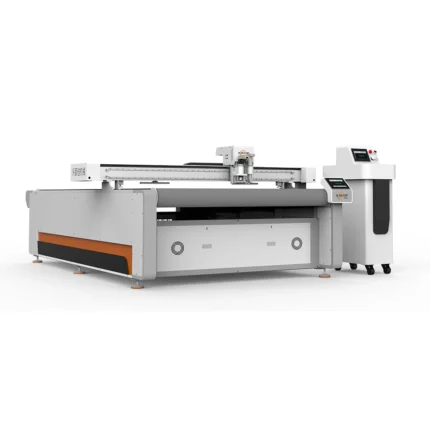
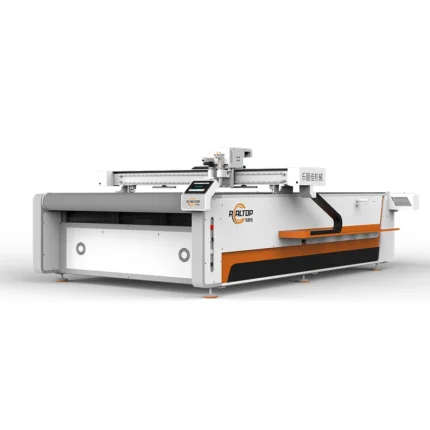
RT-D2516/RT-S2516 Cloth CNC Cutting Machine, 1600×2500mm Working Area, 9kw — engineered for multi-layer fabric, leather, and composite material processing with Swiss imported oscillating knife technology.
This system delivers clean physical cuts with no burnt edges or discoloration, addressing the gap where laser power falls short on heat-sensitive flexible materials. The magnesium-aluminum vacuum table with zoned adsorption holds nested small parts securely, while CCD contour recognition tracks printed marks for precise fabric and sticker cutting.
Sample cutting reports on your specific material verify achievable thickness, edge quality, and cutting speed before commitment, with tool head configuration matched to your production volume and HP-GL file compatibility confirmed.
Swiss Knife Assembly on a Dual-Head Gantry — the oscillating blade mounts directly into a rigid multifunctional head, eliminating the deflection that causes ragged edges on multi-layer technical textiles.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | RT-D2516/RT-S2516 |
| Working Area | 1600 × 2500 mm |
| Machine Size | 3450 × 2300 × 1250 mm |
| Rated Power | 9 kW |
| Table Type | Flat vacuum working table with auto feeding |
| Multifunctional Head | Swiss imported knife: vibration full cutting, vibration half cutting, cursor location |
| Safety Device | Infrared sensors, anti-collision beam, emergency stop with in-situ resume |
| Translational Velocity | 800–2000 mm/s |
| Cutting Speed | 200–800 mm/s (according to different cutting materials) |
| Repeated Accuracy | ≤0.1 mm |
| Transmission System | Digital servo motor, linear guide, synchronous belt, ball screw |
| Instruction System | HP-GL compatible format |
| Voltage | 380V ± 10% |
| Vacuum Pump | 7.5 kW |
| Cutting Thickness | ≤100 mm (varies with the material) (basis not stated in source) |
| Control Language Options | English, Russian, Italian, Chinese (special languages can be customized) |
Application Suitability
| Application | Material or Output |
|---|---|
| Garment and footwear production | Multi-layer clothing cloth, shoe material, non-woven fabric |
| Automotive interior trimming | Sponge composite leather, PU, EVA, XPE |
| Soft home furnishings and carpets | Fabric, textile, carpet, sponge |
| Packaging and signage prototyping | Corrugated cardboard, sticker, film, PVC, plastic box |
| Sealing and gasket fabrication | Rubber, PTFE, ETFE, gasket material |
Why "200–800 mm/s Cutting Speed" Means Nothing Without the Material Stack
The speed figure only holds when the material type, layer count, and blade oscillation frequency are matched to the job.
Buyers often see a wide speed range quoted on a Cloth CNC Cutting Machine and assume the top end applies to their daily work. In reality, cutting a single layer of woven polyester at 800 mm/s is straightforward, but driving that same blade through fifty layers of dense sponge composite leather at the same pace will crush the bottom plies and shift the cut line. The oscillation frequency and the downward pressure must be tuned to the specific stack [NEED_CITE: oscillating knife cutting parameters for multi-layer technical textiles]. On the shop floor, the difference between a clean edge and a fused, ragged section often comes down to a five percent adjustment in blade stroke, not the travel speed on the screen.
How the 10.6-Micron Wavelength Defines Your Material Ceiling
A CO2 laser cutting and engraving machine operates at a wavelength that non-metals absorb readily, which is why it seals the edge of synthetic fabrics as it cuts. That thermal sealing prevents fraying on materials like nylon and polyester, but it also leaves a hardened, sometimes discolored margin on heat-sensitive textiles. When the brief calls for a soft hand-feel on a garment hem or a clean, unburnt edge on a multi-layer foam layup, the thermal process becomes a limitation rather than a benefit. The oscillating knife on the RT-D2516/RT-S2516 bypasses that thermal boundary entirely, leaving the fiber structure untouched.
When Continuous Power Ratings Fall Short on Thicker Layups
Laser tubes are frequently rated at peak output rather than continuous working power, and that gap widens as the material stack grows deeper. A tube that slices cleanly through three millimeters of acrylic at its rated wattage may struggle to maintain a consistent kerf through twenty millimeters of compressed foam, because the assist gas cannot clear the molten debris from a deep, narrow channel [NEED_CITE: CO2 laser continuous versus peak power cutting depth limitations]. Physical blade cutting maintains a constant kerf width regardless of stack depth, provided the vacuum table holds the bottom ply flat and the blade stroke exceeds the total material thickness.
Reading the Specs That Actually Govern Edge Quality
The 7.5 kW vacuum pump and the flat vacuum working table work together to pin the material down; without sufficient hold-down force, the oscillating knife lifts the top plies on the return stroke, creating a stepped edge across the layup. The repeated accuracy of ≤0.1 mm depends directly on the Taiwan Hiwin linear rails and the digital servo motors maintaining positional tolerance under the lateral load of a blade penetrating dense composite leather. The Swiss imported knife head offers vibration full cutting and half cutting in the same setup, which means a single tool path can score a crease line and then cut through the full thickness without a tool change, preserving registration across complex nesting layouts. The 9 kW rated power covers the servo drives, the vacuum pump, and the auto feeding conveyor simultaneously, so the machine does not drop speed when the conveyor engages mid-cycle.
The Cost of Specifying a Machine on Working Area Alone
Purchasing a cutter based solely on bed size leads to problems that only appear once production starts. A buyer who needs to cut sixty layers of automotive headliner foam may find that the machine’s maximum cutting thickness cannot accommodate the compressed stack, or that the vacuum zoning is too coarse to hold small nested parts flat against the table [NEED_CITE: vacuum table zoning requirements for small nested parts in digital cutting]. The result is material lift during the cut, missed contours, and a scrap rate that erodes the yield the nesting software promised. These issues are not warranty claims; they are specification mismatches that could have been caught with a sample cutting report on the buyer’s actual material before the order was placed.
Why Sourcing This Cutter from REALTOP Differs
In-house design and production cover both knife and laser cutting technologies, so the cutting method is matched to the material rather than forced into one process. Tool head and table configurations are specified per material and daily volume, ensuring the oscillation stroke and vacuum zoning align with the actual layup. CCD camera positioning is available for printed contour work on textiles and signage films. Software compatibility is confirmed before the order is released, so HP-GL files and nesting workflows integrate without conversion errors. Voltage, language, and specification customization are finalized on the electrical schematic before the machine enters assembly. Sample cutting on the buyer’s own material is conducted before commitment, providing a physical record of edge quality and achievable speed.
Documentation & Verification
- Machine specification sheet listing the 1600 × 2500 mm working area and configured tool heads
- Electrical schematic and voltage confirmation matching the 380V ± 10% supply at your facility
- Tool head and table configuration list matched to your material stack and daily volume
- Sample cutting report on your actual fabric or composite material before dispatch
- Software licence and file format compatibility note confirming HP-GL import and nesting integration
- Operation and maintenance manual with control language set to your preference
Installation, Commissioning & Support
- Floor space must accommodate the 3450 × 2300 mm footprint plus auto feeding conveyor clearance
- Dedicated 380V ± 10% circuit rated for the 9 kW total draw including the 7.5 kW vacuum pump
- Machine ships with the gantry and table as a single assembly; rigging requires overhead crane access
- First-power commissioning includes vacuum zoning calibration against your specific material sheet size
- Operator training covers Swiss knife head blade changes, oscillation frequency tuning, and in-situ resume after emergency stop
- Spare parts list identifies consumable blades, vacuum table seals, and Hiwin rail blocks for local stocking
What We Need to Quote Accurately
Provide the material type, the maximum layer count or total stack thickness, and the sheet dimensions you run most frequently. Confirm the voltage and frequency at your facility, the control language your operators require, and whether your existing nesting software outputs HP-GL or another format. If your production involves printed contours, specify the mark size and contrast so the CCD camera configuration can be validated in advance.
Frequently Asked Questions
Q: How do I verify the 200–800 mm/s cutting speed claim for my material?
A: The speed range depends entirely on the material density, layer count, and blade oscillation frequency. Request a sample cutting report run on your exact fabric or composite layup. That report documents the actual travel speed, edge quality, and blade life achieved under production conditions, replacing generic estimates with measured data you can plan around.
Q: When should I choose this oscillating knife over a CO2 or fiber laser for textiles?
A: Oscillating knife cutting is preferred when the material is heat-sensitive, when multi-layer stacks exceed the practical cutting depth of a laser kerf, or when the edge must remain soft and unburnt for garment assembly. Laser cutting seals synthetic edges, which is an advantage for some applications but a defect for others. The choice is driven by the material response to heat and the required edge finish.
Q: Can the vacuum table hold small nested parts without material lift?
A: The flat vacuum working table is divided into zones that can be activated independently to match the sheet size and the nesting layout. For very small parts, additional hold-down strategies such as masking or reduced oscillation stroke are configured during commissioning. The 7.5 kW pump provides the suction volume needed to maintain hold-down force across the full 1600 × 2500 mm area.
Q: Will the control software accept my existing nesting files?
A: The instruction system is HP-GL compatible, which covers most standard nesting outputs. Before the order is finalized, your file format and workflow are tested against the machine’s software to confirm import, tool path assignment, and contour recognition. Any required conversion or post-processor adjustment is documented in the software compatibility note shipped with the machine.
Q: What voltage and language options are confirmed before shipment?
A: The standard electrical supply is 380V ± 10%, but the machine can be configured for other industrial voltages. The control interface is available in English, Russian, Italian, and Chinese, with other languages customizable. Both the voltage and the language are locked in on the electrical schematic and specification sheet before the machine enters production, ensuring the installation matches your facility and your operators.


Related products
2026 Automatic PVC Tarpaulin Cutter Machine
Product Introduction
High-performance Automatic PVC Tarpaulin Cutter Machine 2026, ideal for precise and efficient cutting of PVC tarpaulin materials, designed for industrial manufacturing needs with reliable operation and user-friendly control.Product Parameters
| Model | 2026 |
| Type | Automatic PVC Tarpaulin Cutter |
| Application | PVC Tarpaulin Cutting |
| Feature | Precise & Efficient Cutting |
2026 CNC Knife Cutting Machine for Fabric Leather PVC Hot Sale
Product Introduction
2026 Hot Sale CNC Knife Cutting Machine for Fabric, Leather, PVC. Ideal for precise cutting of various materials with advanced CNC technology, perfect for manufacturing needs.
Product Parameters
| Application | Fabric, Leather, PVC |
| Type | CNC Knife Cutting Machine |
| Feature | Precision Cutting |
| Year | 2026 Model |
2026 Inflatable Surf SUP Board Cutting Machine
Product Introduction
Ideal for inflatable surf SUP board production, this 2026 cutting machine ensures precise and efficient cutting, tailored for manufacturers seeking reliable performance in water sports equipment manufacturing.
Specifications
| Application | Inflatable Surf SUP Board |
| Type | Cutting Machine |
| Model Year | 2026 |
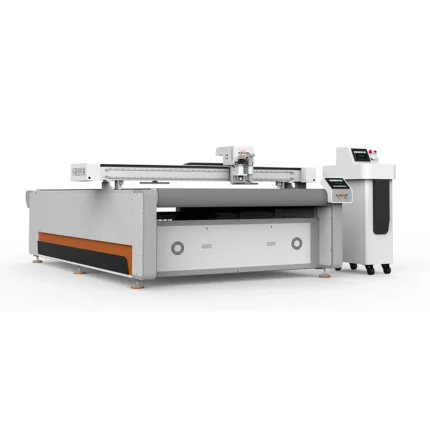
CNC Oscillating Knife Cutting Machine 2026 3000¡Á1600mm High-Speed
Product Parameters
| Model | CNC Oscillating Knife Cutting Machine 2026 |
| Working Area | 3000mm¡Á1600mm |
| Cutting Type | Oscillating Knife |
| Application | Fabric Cutting |
| Feature | High-Speed |
Introduction
High-performance CNC oscillating knife cutting machine with 3000mm¡Á1600mm working area, ideal for high-speed fabric cutting. Precision and efficiency for professional textile processing needs.
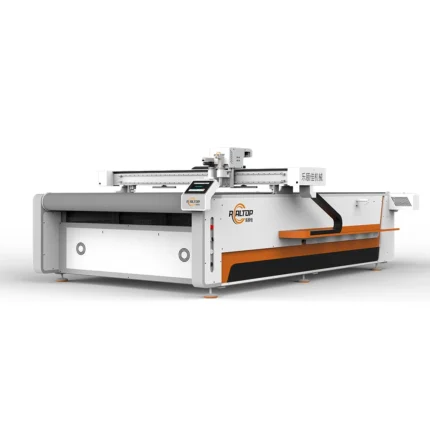

Electric Fabric Rotary Cutter 2026 12V Auto-Cut Industrial
Product Introduction
Industrial-grade Electric Fabric Rotary Cutter designed for precise cutting of scan-printed cloth. Features 12V auto-cut functionality for efficient, automated operation, ideal for professional textile processing.Product Parameters
| Power Supply | 12V |
| Function | Auto-Cut |
| Application | Scan-Printed Cloth |
| Type | Industrial Electric Rotary Cutter |
商品评价
There are no reviews yet.