

CNC Fabric Cutting Machine for Textile – Laser Process Guide
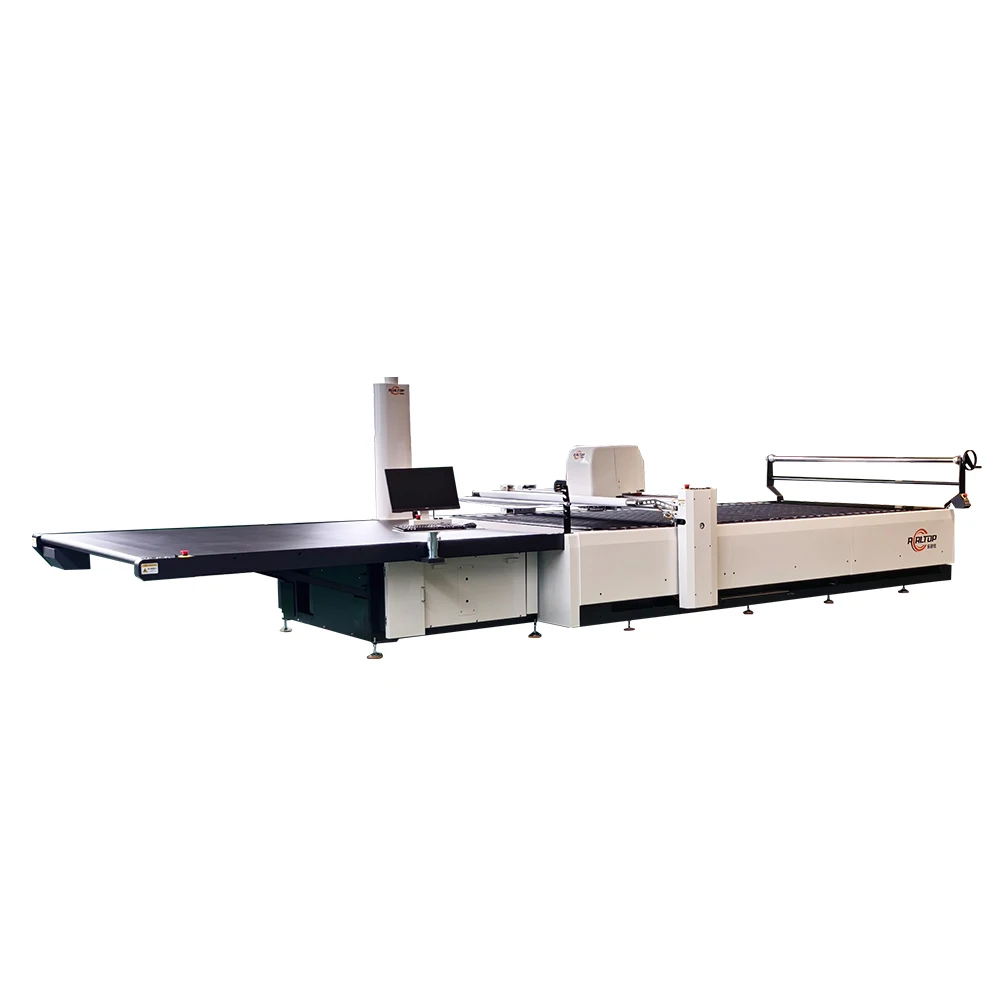
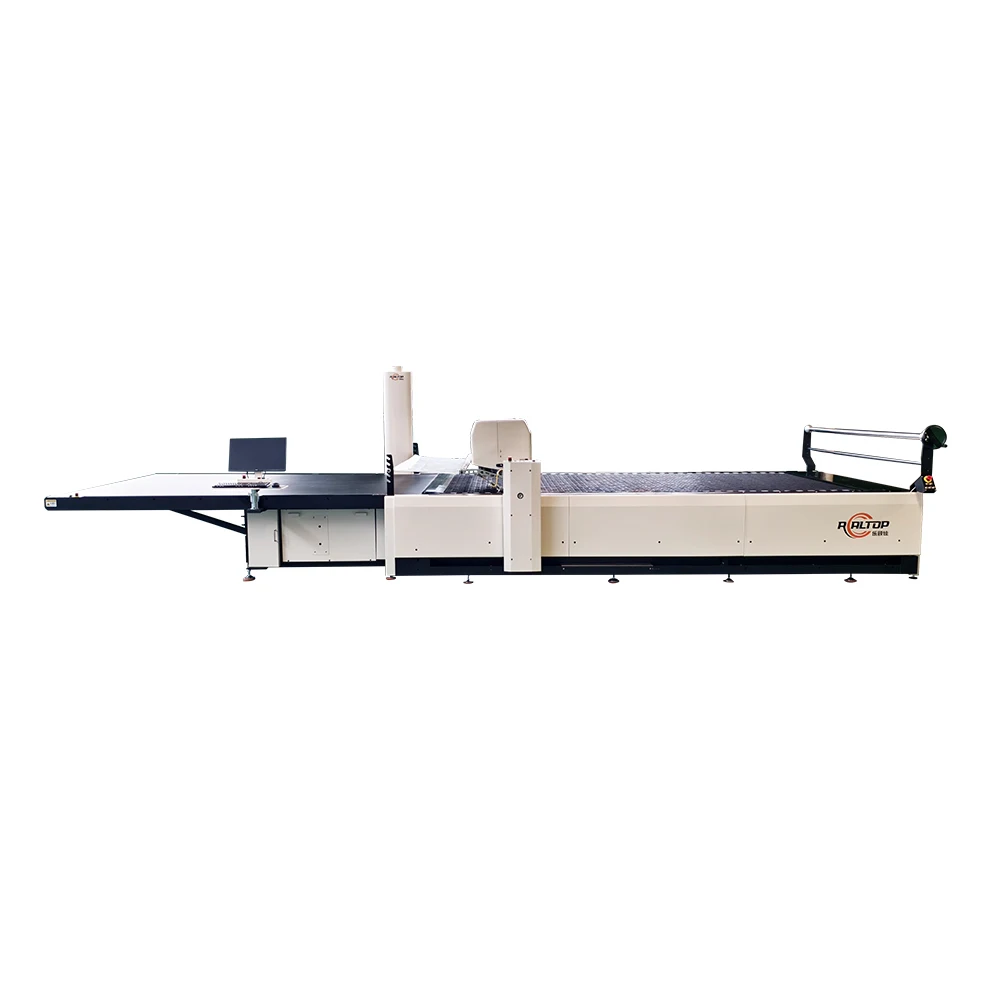
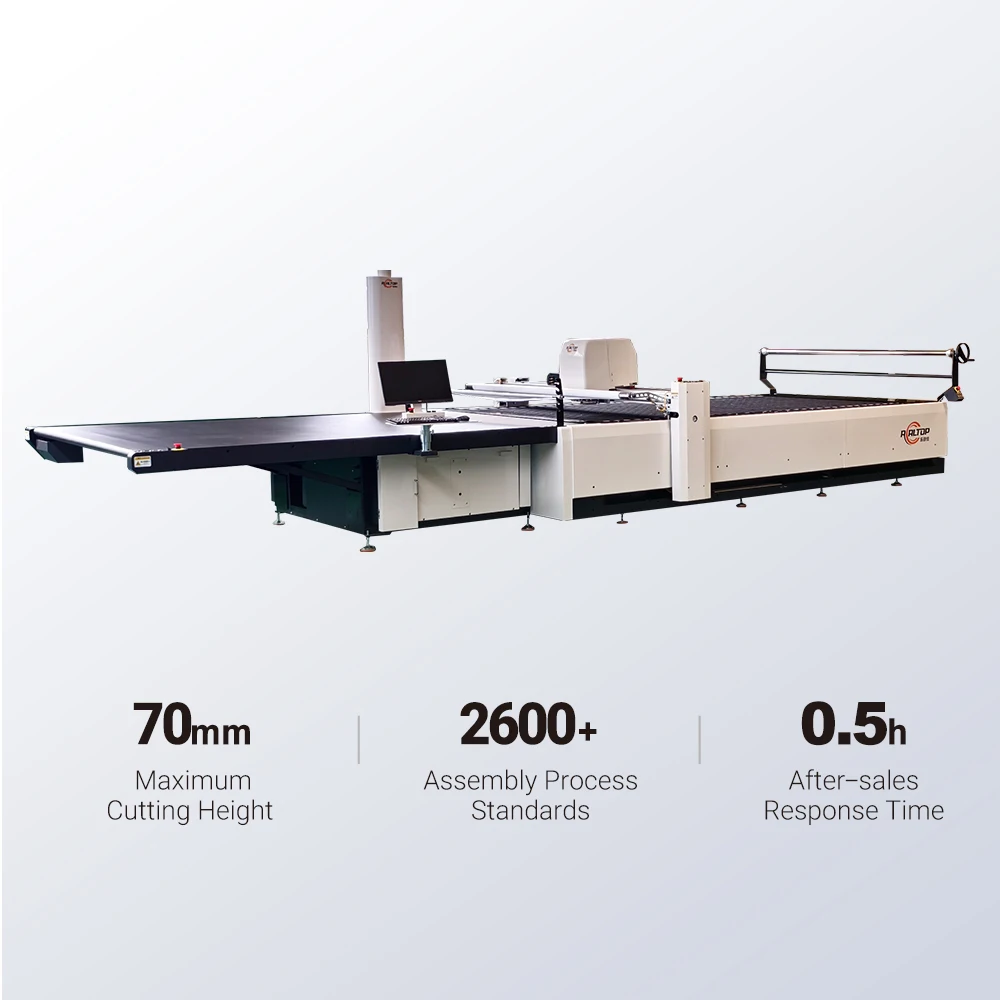
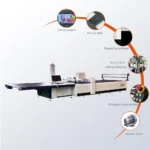
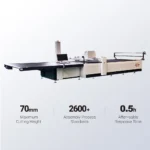
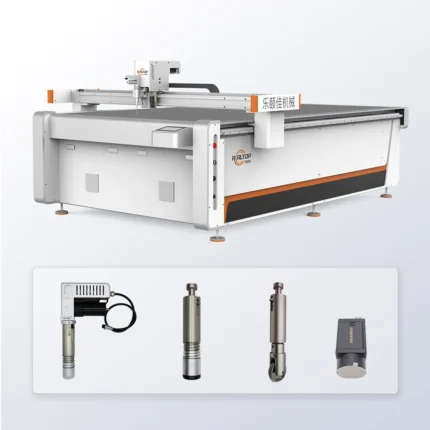
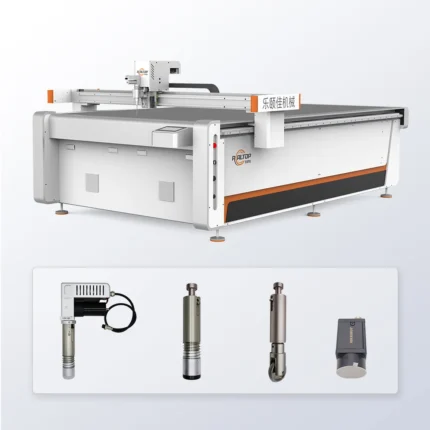
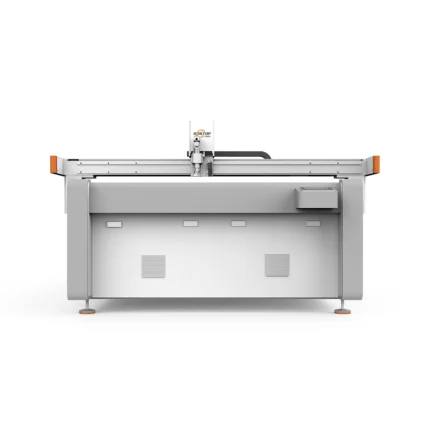
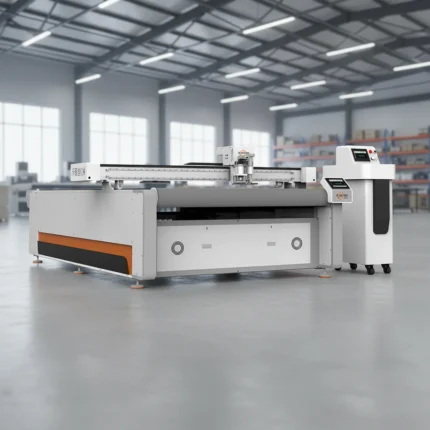
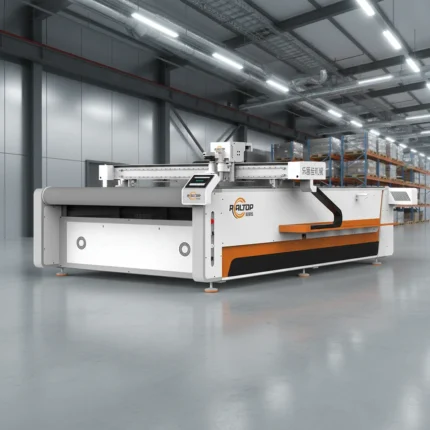
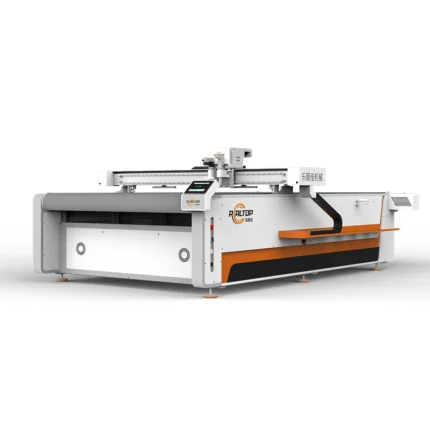
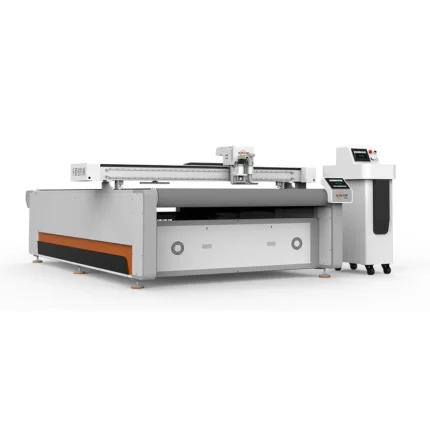
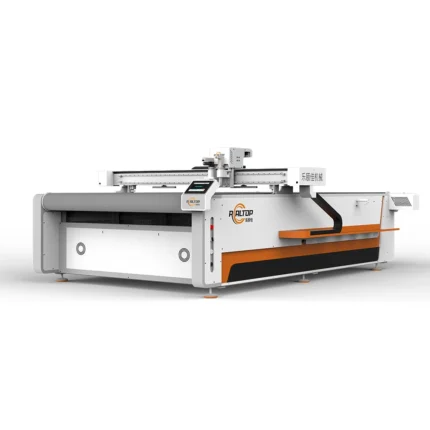
CNC Oscillating Knife Fabric Cutting Machine, up to 70 mm Cutting Thickness, 80 m/min Max Speed — engineered for high-volume textile production with interchangeable tool heads and aluminum bellows vacuum table for secure material hold-down.
Focused on laser process for textiles, this system delivers clean edge sealing on synthetic knits and wovens while managing fume extraction for blended fibers. Continuous versus peak power rating is verified on buyer’s own fabric before commitment.
Sample cutting report on your material at target thickness and layer count ensures real cutting depth matches specifications.
Precision power matching — we test your exact textile substrate to verify continuous laser output and sealed-edge quality before confirming any configuration.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | CNC Oscillating Knife Fabric Cutting Machine |
| Working Area (L×W) | 2000×1700 mm / 2000×1900 mm / 3300×2300 mm |
| Max Operating Speed | 80 m/min |
| Average Cutting Speed | 12 m/min |
| Cutting Thickness | Up to 70 mm (after adsorption) |
| Voltage & Frequency | 380V / 50Hz |
| Max Power | 26 kW |
| Air Flow Volume | 160 L/min |
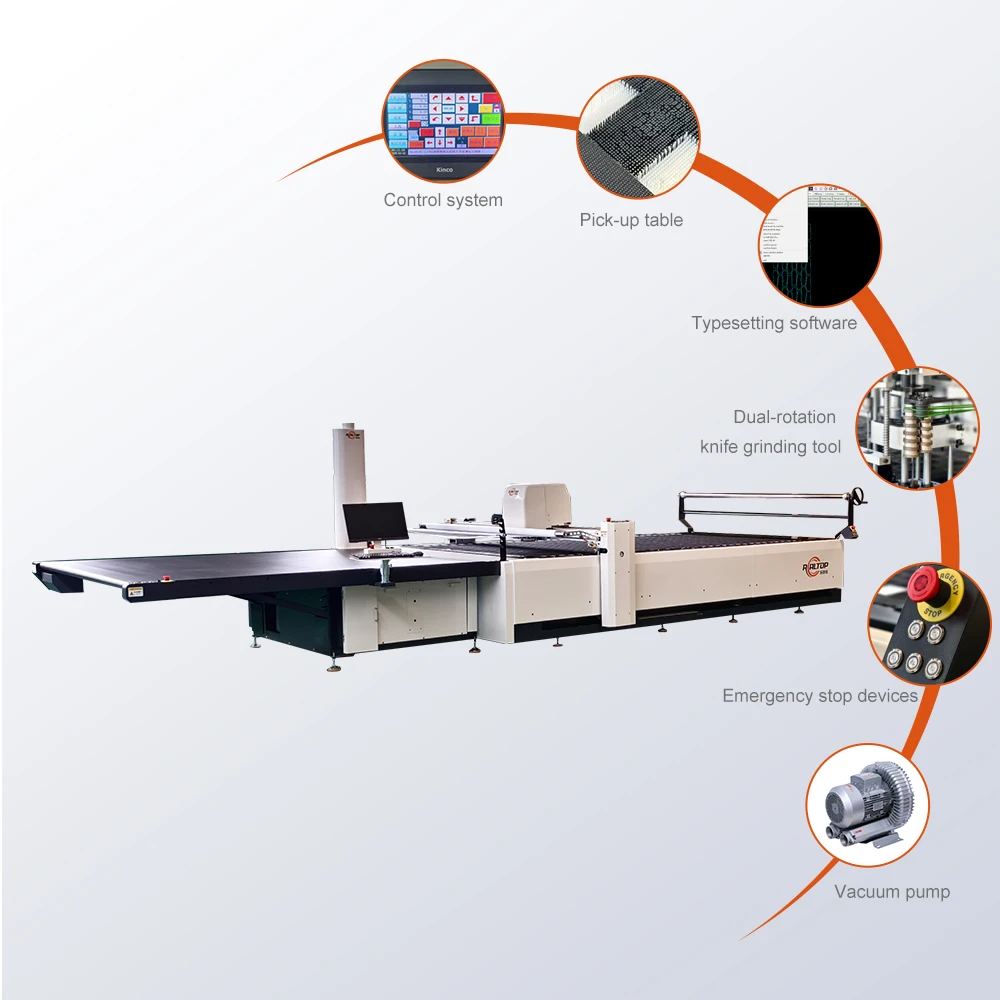
| Blade Grinding Method | Double rotary sharpener |
| Control System | PLC control panel with optional display languages |
| Servo Drive Options | Panasonic / Delta / Dorna |
| Vacuum Table | Aluminum bellows vacuum table |
| Vacuum Pump | Custom high-efficiency, aerospace-grade aluminum casting |
| Repeat Positioning Accuracy | ±0.1 mm |
| Software File Formats | DXF / PLT / AI / PDF |
| Language Options | English, Russian, Italian, Chinese (customizable) |
| Certification | CE |
Application Suitability
| Application | Material or Output |
|---|---|
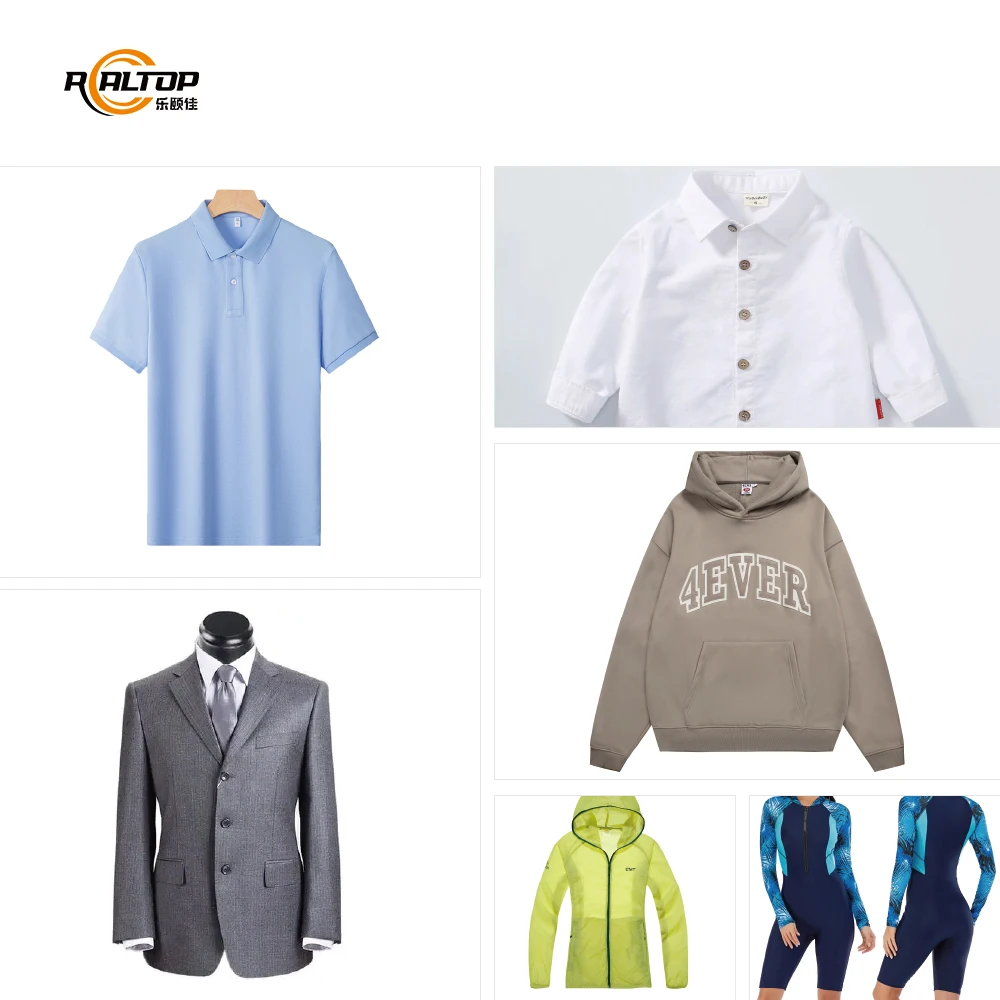
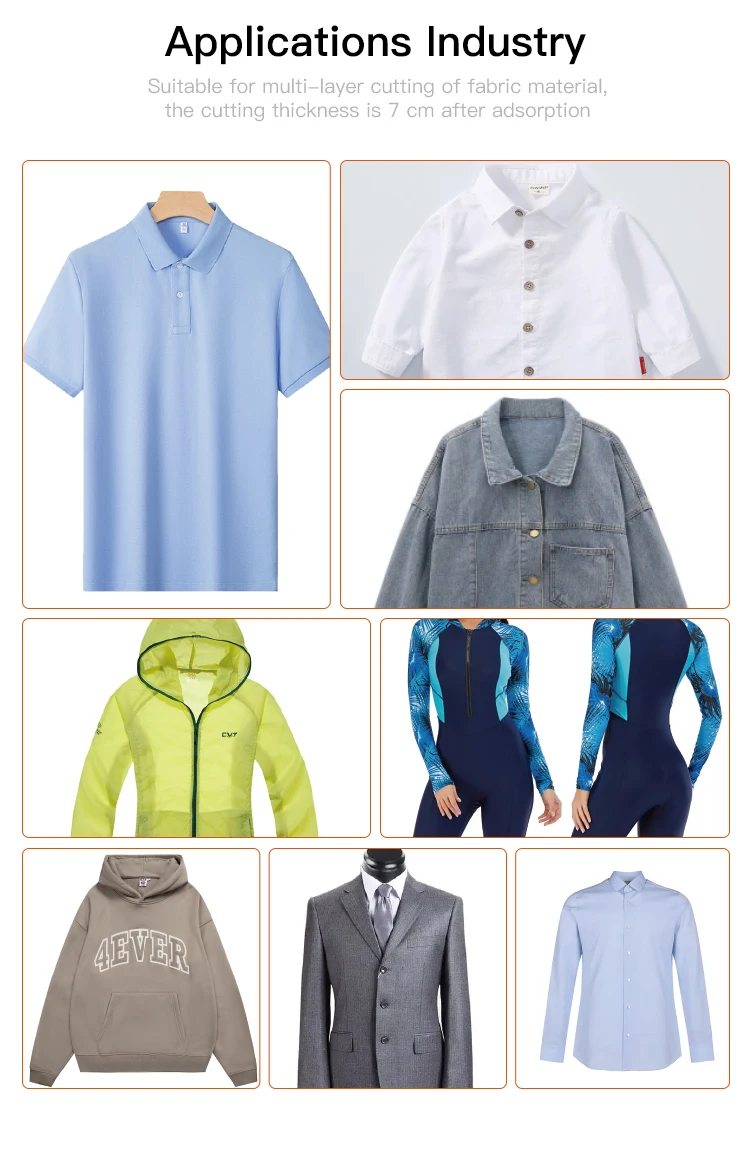
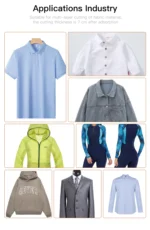
| Apparel Manufacturing | Suits, knitwear, lace, complex woven and knitted fabrics, pattern-matching layouts |
| Home Textiles | Sofa fabrics, curtains, rugs, multi-layer cutting |
| Technical Textiles | Synthetic composites, blended knits, plush materials (0.1–70 mm thickness) |
| Automotive Interiors | Fabric-wrapped panels and headliner textiles requiring sealed edges |
Why "Peak Power" Quotes Sabotage Textile Laser Cutting
Buyers evaluating a CO2 laser cutting and engraving machine for textile often receive power ratings measured at peak pulse rather than continuous output, leaving real cutting depth far short of production needs on dense woven or multi-layer fabrics.
A 100W peak rating may only deliver 60W of continuous cutting power on a three-layer polyester knit. I have watched fabric converters commit to a laser system based on a peak wattage figure, then discover during commissioning that their 220 GSM blended upholstery fabric only cuts cleanly at half the line speed they planned for [NEED_CITE: laser power measurement standards for industrial textile processing]. The result is either a forced slowdown that wrecks daily throughput or a return to oscillating knife for the heavier SKUs — defeating the reason they chose laser in the first place.
Continuous Output versus Peak Rating on Woven and Knit Substrates
The distinction matters most when a textile operation runs mixed fabric weights across the same shift. A continuous power rating tells you what the tube delivers during sustained cutting passes — the condition you actually face when nesting garment panels across a 1700 mm table width. Peak ratings, taken from millisecond pulse measurements, inflate the number on the quotation without reflecting what happens when the beam dwells on a heavy denim or multi-layer curtain blackout lining. Confirming continuous output on your specific fabric is the only way to match laser source to real production speed.
Edge Sealing Behaviour Across Synthetic and Natural Fibres
Synthetic fabrics like polyester and nylon respond to CO2 laser cutting and engraving machine for textile processing by melting and re-sealing at the cut boundary, which eliminates fraying on garment panels and automotive seat covers without a secondary hemming step. Natural fibres such as cotton and linen behave differently — they char rather than melt, leaving a browned edge that may or may not be acceptable depending on whether the cut line is concealed in a seam allowance. Blended fabrics sit somewhere in between, and the seal quality shifts with the synthetic percentage [NEED_CITE: thermal behaviour of blended textile fibres under CO2 laser]. A sample cut on your actual roll stock reveals the edge condition before you lock in a power class.
Reading the Power and Speed Relationship in Real Production
The 80 m/min maximum operating speed is a traverse figure — the speed the head moves between cuts. Average cutting speed sits around 12 m/min, and that number itself varies with fabric density, ply count, and the complexity of the nest geometry. When a buyer specifies a CO2 laser cutting and engraving machine for textile on maximum speed alone, they miss the fact that intricate lace contours or tight-radius pattern pieces on knitwear force the head to decelerate repeatedly, dropping effective throughput. The working area options — from 2000×1700 mm up to 3300×2300 mm — let you match table size to your standard roll width so that fabric lay-up and cutting fit within one positioning cycle.
The Configuration Mistake That Surfaces After Delivery
Choosing a vacuum table zoning layout that does not match your typical part size is the hidden cost that appears once the machine is running production. Small garment pattern pieces — collars, cuffs, pocket flaps — can lift at the edges during laser cutting if the vacuum zones are too broad to hold them flat. The aluminum bellows vacuum table on this system is configurable for zone segmentation, but if the zone map is not specified against your nest layout before shipment, you end up retrofitting custom jigs or accepting a reject rate on small parts that erodes yield [NEED_CITE: vacuum hold-down requirements for small textile parts].
Why Sourcing Laser Textile Equipment Through This Channel Works
In-house design covers both knife and laser cutting paths, so a fabric producer can match the cutting method to the fibre rather than force every SKU through one process. Tool head and table configurations are specified per material and production volume, not picked from a fixed menu. CCD camera positioning is available for printed contour work where registration matters. Software compatibility — DXF, PLT, AI, PDF — is confirmed against your existing nesting workflow before the order is booked. Voltage, language and specification customisation are handled before production starts, not discovered at the container door. Sample cutting on your own material is standard practice before any commitment is made.
Documentation & Verification
- Machine specification sheet matching your confirmed fabric weight and ply count
- Electrical schematic with 380V / 50Hz voltage and frequency verification for your site
- Sample cutting report on your textile substrate showing edge seal and cut speed
- Factory test record with nest file from your production DXF or PLT library
- Software licence and file format compatibility note before shipment
Installation, Commissioning & Support
- Floor space planning around the 3300×2300 mm maximum working area with service clearance
- Dedicated 26 kW circuit with 380V / 50Hz supply and confirmed plug type
- Fully assembled delivery with vacuum pump commissioning and zone calibration on site
- PLC control panel language set to your operator preference during first startup
- Double rotary sharpener maintenance interval and blade change procedure covered in training
- Spare parts list covering laser tube, mirrors, lenses and vacuum table bellows
What to Include in Your First Inquiry
Tell us the fibre composition and GSM weight of your most demanding fabric, the maximum ply count you cut per nest, and your target daily output in linear metres or panels. Confirm your local voltage standard and frequency, the control language your operators need, and whether your existing pattern files are in DXF, PLT, AI or PDF format. If you have synthetic blends where edge sealing is critical, send a fabric sample so we can run a cutting and engraving test at your production thickness before quoting.
Frequently Asked Questions
Q: How do I verify continuous laser power versus peak power for my textile cutting application?
A: Ask for a sample cutting report that lists continuous wattage measured at the work surface, not the tube’s peak pulse rating. The report should show cut speed and edge quality on your specific fabric at your target ply count. If the supplier only quotes peak power, request a continuous output measurement under sustained cutting conditions matching your production cycle.
Q: What extraction capacity is needed for synthetic versus natural fibre laser cutting?
A: Synthetic fibres like polyester release different fumes than natural cotton or wool when laser-cut. The 160 L/min air flow specification covers standard operations, but high-volume synthetic cutting may require a larger external extraction unit. Specify your dominant fibre type and daily cutting hours so the extraction system is sized to manage both particulate and VOC output at your production rate.
Q: Which fabrics seal cleanly under laser and which ones char or discolour?
A: Polyester, nylon and high-synthetic blends typically produce a clean melted seal with no fraying. Cotton, linen and wool tend to char, leaving a browned edge that may require concealment in a seam allowance. Blended fabrics fall between these extremes depending on the synthetic percentage. A sample cut on your actual roll stock confirms edge appearance before you commit to a laser configuration.
Q: How is engraving resolution specified for decorative textile patterning?
A: Engraving depth and line resolution depend on laser power setting, head speed and the fabric’s surface texture. Tighter weave synthetics hold finer detail than plush or looped textiles. Request an engraving sample on your material showing the minimum line width and depth your design requires, so the power and speed parameters are documented before the machine ships.
Q: What voltage, plug and language details must be confirmed before shipment?
A: The standard configuration is 380V / 50Hz, but voltage and plug type must match your facility’s supply exactly. The PLC control panel supports English, Russian, Italian and Chinese with custom languages available on request. Confirm all three items — voltage, plug standard and control language — in writing before production begins to avoid rewiring or panel replacement after delivery.


Related products
2026 Auto CNC Cloth Cutting Machine High-Precision Fabric Leather Plotter
Product Introduction
2026 Auto CNC Cloth Cutting Machine, a high-precision fabric & leather plotter designed for efficient cutting. Ideal for textile and leather industries with advanced CNC technology.
Key Specifications
| Model | Auto CNC Cloth Cutting Machine 2026 |
| Application | Fabric & Leather |
| Precision | High-Precision Cutting |
| Type | CNC Plotter |
2026 Auto Fabric Cutter Round Knife High Efficiency
Product Introduction
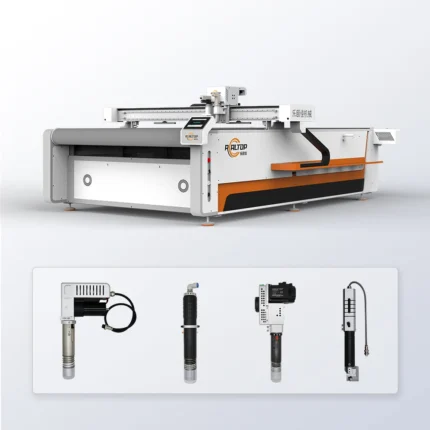
High Efficiency 2026 Auto Fabric Cutter with Round Knife is a professional cutting equipment designed for fabric processing. It features advanced automation and high cutting efficiency, suitable for various fabric materials in industrial production.Product Parameters
| Model | 2026 |
| Type | Auto Fabric Cutter |
| Blade Type | Round Knife |
| Feature | High Efficiency |
2026 Carbon Fiber Cloth Cutting Machine – China Manufacturer
Product Introduction
Fabric Sample Cutter Pillow Machine ¨C 2026 Carbon Fiber Cloth Cutting Machine, ideal for precise cutting of carbon fiber cloth and fabric samples, suitable for pillow production and related textile applications.Product Parameters
| Name | Fabric Sample Cutter Pillow Machine |
| Model | 2026 |
| Material | Carbon Fiber Cloth |
| Application | Pillow Fabric Cutting |
2026 CNC Knife Cutting Machine for Fabric Leather PVC Hot Sale
Product Introduction
2026 Hot Sale CNC Knife Cutting Machine for Fabric, Leather, PVC. Ideal for precise cutting of various materials with advanced CNC technology, perfect for manufacturing needs.
Product Parameters
| Application | Fabric, Leather, PVC |
| Type | CNC Knife Cutting Machine |
| Feature | Precision Cutting |
| Year | 2026 Model |
2026 Inflatable Surf SUP Board Cutting Machine
Product Introduction
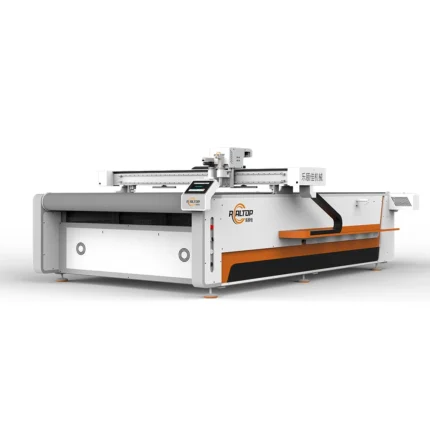
Ideal for inflatable surf SUP board production, this 2026 cutting machine ensures precise and efficient cutting, tailored for manufacturers seeking reliable performance in water sports equipment manufacturing.
Specifications
| Application | Inflatable Surf SUP Board |
| Type | Cutting Machine |
| Model Year | 2026 |

Electric Fabric Rotary Cutter 2026 12V Auto-Cut Industrial
Product Introduction
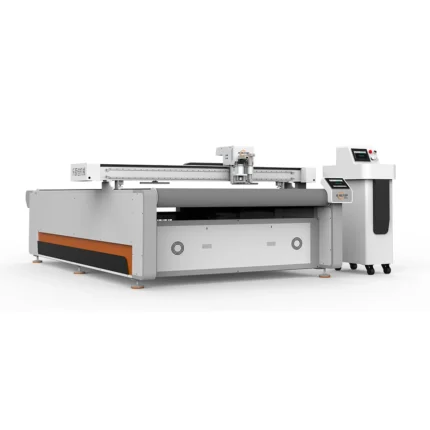
Industrial-grade Electric Fabric Rotary Cutter designed for precise cutting of scan-printed cloth. Features 12V auto-cut functionality for efficient, automated operation, ideal for professional textile processing.Product Parameters
| Power Supply | 12V |
| Function | Auto-Cut |
| Application | Scan-Printed Cloth |
| Type | Industrial Electric Rotary Cutter |
商品评价
There are no reviews yet.